
A molded sports-equipment shell may protect a sensor, guide a strap, carry a fastener, provide a grip surface or form the visible identity of a product. A bicycle accessory cover, training-device housing, protective guard or racket-related component can look simple in CAD while carrying very different impact, fatigue, weather and assembly risks. A quote based only on part weight and annual volume leaves those risks for the sample stage, when a gate, texture or material decision may already be expensive to change.
For buyers, the useful question is not simply which resin or supplier can mold a shell. It is whether the RFQ explains the actual load cases, repeated-use expectation, mating parts, cosmetic zones, texture intent and acceptance evidence. InjeForm's [industrial equipment application page](/products/industrial-equipment) is a relevant starting point for durable covers, guards and mounting features; send the controlled package through [request a quote](/request-a-quote) for a part-specific review.
Buy the shell as a tested interface: define the impact event, fatigue cycle, grip or texture purpose, assembly load and inspection method before comparing unit prices.
01
1. Describe the sports product and its real duty cycle
Start the RFQ with the product context, not just the exterior shell. Identify whether the part is a protective cover, handle housing, guard, frame-side enclosure, equipment cap, sensor cover or user-contact trim. Show the internal components, strap or buckle, fasteners, inserts, seals, foam, electronics and neighboring parts. Mark what the shell must protect, what may contact the athlete or ground, and whether the product is expected to be opened, serviced or replaced.
Translate use into load cases that can be discussed and tested. State likely drop or impact orientations, repeated flexing or button cycles, fastening torque, strap pull, vibration, UV or moisture exposure, temperature range, sweat or cleaning-agent contact and storage conditions where relevant. Do not turn a generic impact-resistance label into a performance guarantee: the product owner should define representative energy, fixture, conditioning and pass/fail criteria for the finished assembly.
Include demand by product version, launch and ramp assumptions, color or finish variants, packaging, target markets and whether the tool may be transferred. Ask the supplier to list assumptions for gate location, parting line, cavity count, inserts, secondary assembly and inspection. This makes a sports-shell quote comparable without pretending that a preliminary design review has already proven field durability.
| RFQ input | What to provide | Risk it helps expose |
|---|---|---|
| Use and load cases | Drop direction, impact object, repeated flexing, strap pull, torque, vibration and environmental conditions | A shell qualified for appearance but not for the way athletes handle it |
| Assembly stack | Mating shell, liner, insert, buckle, strap, fastener, seal, electronics and build sequence | Cracked bosses, trapped parts, poor closure or inaccessible assembly |
| Appearance and touch | Visible zones, approved color, gloss, texture purpose, grip requirement and blemish boundaries | A cosmetic finish that conflicts with draft, ejection or tactile function |
| Program demand | Variants, annual volume, ramp profile, cavity expectation, packaging and target release | Tooling or capacity assumptions that do not match the product plan |
| Acceptance evidence | CTQs, fixtures, conditioning, sample quantity, functional tests and records | Disputes over whether a sample is impact-, fatigue- or assembly-ready |
02
2. Ask how the shell will manage impact without hiding weak points
Impact performance is a system property, not a polymer name. Review shell thickness transitions, corners, ribs, bosses, windows, vents, fastener seats and attachment points together. A sharp inside corner or a heavy boss can concentrate stress; a weld line near a latch or mounting ear may deserve a targeted review; and a gate vestige or ejector mark on a contact surface can become a crack starter or handling issue. InjeForm's [DFM and mold-design service](/injection-mold-design-dfm) can help turn these locations into marked-up design decisions before steel is cut.
Ask the supplier to show flow direction, likely weld-line locations, gate and vent strategy, ejection forces and the relationship between ribs and the show surface. For glass-filled grades, discuss fiber orientation and directional shrinkage rather than assuming that more reinforcement automatically improves a shell. For unfilled or impact-modified grades, ask how wall geometry, temperature, conditioning and assembly stress affect the intended result. The exact resin grade and supplier data remain necessary inputs.
Define impact evidence around the finished product's credible failure modes. A drop test may be appropriate for one product, while a guarded impact, puncture, latch breakage or retained-component check may matter for another. Specify the assembly configuration, conditioning, impact location, striker or surface, number of samples and acceptance criteria through the product validation plan. A supplier's material datasheet or a clean visual sample is not proof of shell-level impact performance.
03
3. Treat fatigue, fasteners and assembly as one design problem
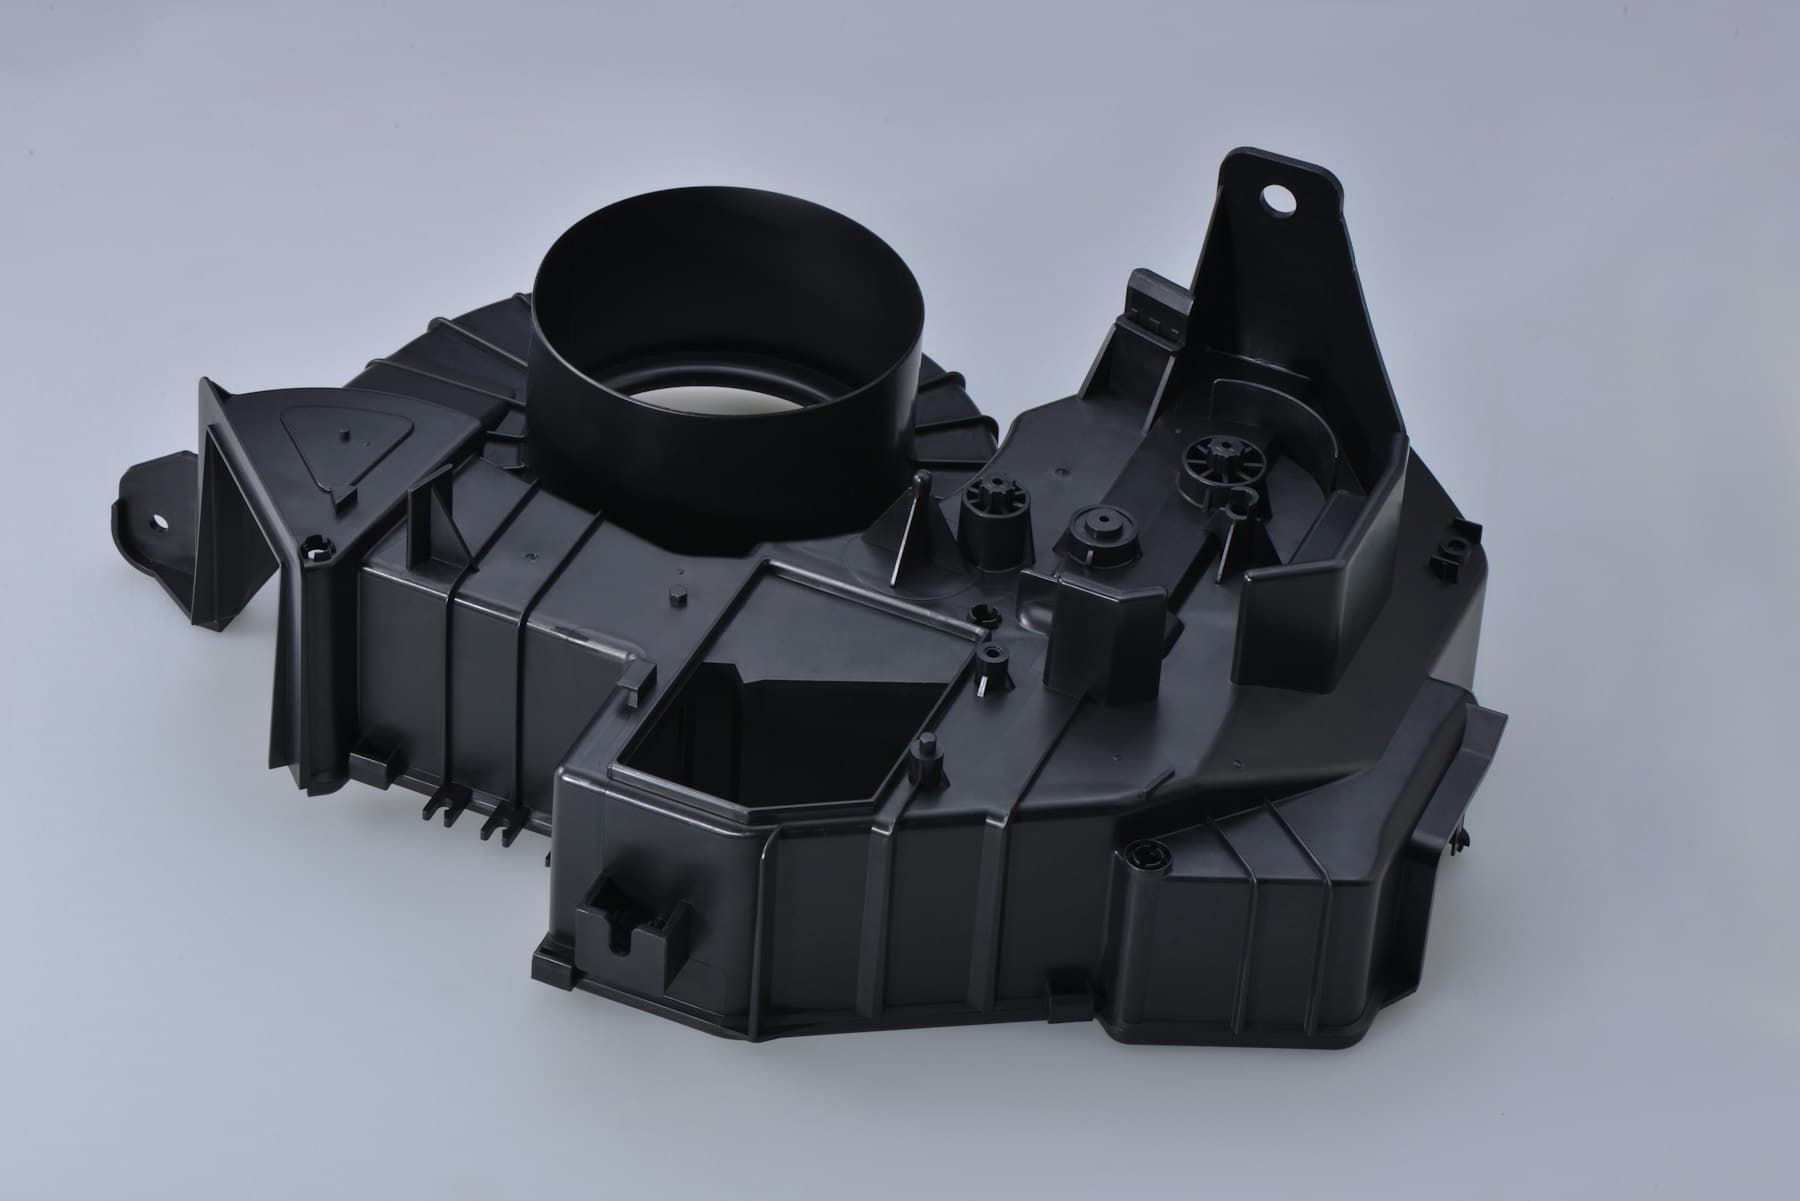
Sports products are often handled repeatedly: covers are opened, straps are tightened, clips are snapped, buttons are pressed and equipment is dropped or vibrated during transport. Identify every feature that sees repeated stress, including snap arms, hinge roots, screw bosses, buckle towers, handle transitions and insert interfaces. State the intended cycles, assembly speed, service access and whether a user can re-tighten or replace a component. The buyer or product owner should set durability targets; the molder can propose geometry and process controls to support them.
Review the assembly sequence with actual mating parts. Check screw boss support, insert seating, torque or press-fit force, clip engagement, clearance for tools, gasket compression, strap alignment and the possibility of partial engagement. A thicker feature may improve local stiffness but create sink, warpage or a mismatch with the mate. A snap can pass a one-time insertion check and still fail after repeated cycling. Request both dimensional evidence and the functional test that represents the assembly risk.
Compare molded-in inserts, post-mold hardware, ultrasonic or heat-staked closures and separate fasteners against volume, repairability, corrosion exposure, tolerance stack-up and traceability. Ask how wrong-part loading, missing inserts, cross-threading, flash and damaged shells are detected. Link the production control plan to the actual assembly characteristic: vision may confirm presence, but torque, pull, retention, closure or cycle testing may be needed to demonstrate function.
| Construction choice | Buyer question | Evidence before release |
|---|---|---|
| Snap-fit shell | What are insertion, retention, removal and cycle expectations? | Sectioned DFM, force or retention method, cycle result and post-test inspection |
| Screw or threaded boss | What torque, clamp load, insert and rework assumptions apply? | Boss and insert dimensions, torque window, strip or pull-out plan and assembly records |
| Strap or buckle mount | Where does the load enter the shell and how is it distributed? | Mating-part fit, pull or load test defined by the product owner, and failure review |
| Two-shell closure | How are alignment, seal, fasteners and service access controlled? | Assembly fixture or gauge, gap and flush checks, closure function and revision traceability |
04
4. Specify texture and material by purpose, not shorthand
Texture can mask handling marks, reduce perceived gloss, support grip, manage reflection or create a brand surface. It also changes draft, release force, tool finishing, measurement and the way a blemish is judged. Mark texture by surface zone and purpose, identify the reference system or approved plaque, and state the viewing or tactile method. Terms such as matte, rubberized or sports grip are not complete acceptance criteria. InjeForm's [injection mold making capability](/injection-mold-making) can be evaluated against the required mold finish and maintenance plan.
Name the exact commercial grade where known, including producer, reinforcement, impact modifier, colorant, UV package, flame-related requirement and approved alternatives. A preliminary screen may include PP for lightweight, flexible or chemical-resistant features; ABS or PC/ABS for rigid cosmetic shells; PA or PA-GF for selected load-bearing details; and TPE for a soft-touch or grip interface. These are directions, not approvals. Compare moisture sensitivity, shrinkage, weld-line behavior, creep, temperature, chemical exposure, color stability and assembly loads for the actual design.
Ask whether texture, color, resin and gate changes alter inspection or durability evidence. A new masterbatch, filler level or recycled-content route can change flow, gloss, shrinkage or fatigue behavior. Require written change control for grade, colorant, texture, tool insert, gate, process window and secondary finish. If the product carries a consumer-safety, sports-standard or market-specific claim, the responsible product authority must determine applicable testing; molding evidence alone does not establish compliance.
05
5. Request configuration-linked evidence and clear supplier answers
Before tooling, ask for a marked DFM covering shell draw direction, parting line, gates, vents, weld lines, ribs, bosses, texture depth, ejection, inserts and assembly access. Ask the supplier to separate tooling, samples, inspection, testing, assembly, packaging and production pricing, and to identify the three assumptions that most influence the quotation. InjeForm's [quality page](/quality) is a useful context for discussing CTQs, sample records and inspection responsibility.
For trials and production release, require the part revision, exact resin and lot, color or additive identity, tool and cavity, process or conditioning state, fixture, measurement method and actual results to travel with the evidence. Dimensional reports should use agreed datums; visual reviews should use the approved sample or plaque; impact, fatigue, retention, torque, closure or pull tests should identify the assembled configuration and test conditions. A first article can support a decision, but it does not replace the product-specific validation plan.
Ask how the supplier controls nonconforming shells, cavity identity, resin drying where applicable, tool maintenance, spare capacity, engineering changes, packaging and export handover. Clarify mold ownership, data access, sample retention, change notification and responsibility for final product validation. Production should release only after the open shell, impact, fatigue, texture and assembly risks have an owner and accepted evidence.

Practical takeaway
Before you move
to the next review.
- Send controlled shell CAD and drawings with mating parts, straps, buckles, inserts, fasteners, seals and the assembly sequence.
- Define representative impact, fatigue, environmental and assembly load cases with conditioning, fixtures, sample quantities and pass/fail ownership.
- Mark cosmetic and grip zones, texture references, color standards, gate or ejector restrictions and the inspection method for appearance.
- Compare exact resin grades and construction options using shrinkage, weld-line, creep, moisture, chemical, temperature and repeated-load evidence.
- Require configuration-linked DFM, trial records, functional tests, traceability, change control, packaging and production-release gates in writing.
FAQ
Common questions
What should a sports equipment shell injection molding RFQ include?
Include controlled CAD and drawings, product duty cycle, impact and repeated-use loads, mating parts, assembly sequence, exact material direction, texture and appearance zones, volume, CTQs, test methods and release timing.
Which plastic is best for a sports equipment shell?
There is no universal best resin. PP, ABS, PC/ABS, PA or PA-GF and TPE may suit different features, but the exact grade must be checked against impact, fatigue, creep, moisture, temperature, chemicals, texture, color and assembly loads.
How should buyers validate impact resistance?
Define the representative product assembly, conditioning, impact location and energy or striker, sample quantity and pass/fail criteria with the product owner. A material datasheet or visual inspection alone does not qualify the finished shell.
Does molded texture improve sports equipment grip?
It can support grip or reduce reflections, but texture is not a universal performance guarantee. Specify the purpose, zone, reference plaque or texture system, draft implications and tactile or visual acceptance method, then test the finished product.
What supplier evidence should precede production release?
Request approved DFM and material records, tool and cavity identity, dimensional results, visual approval, impact or fatigue evidence where required, assembly checks, resin traceability, deviations and a documented change route.
References
Source material
- [1] International Organization for Standardization, ISO 20457:2026 — Plastics moulded parts: Tolerances and acceptance conditions.
- [2] ASTM International, ASTM D256 — Standard Test Methods for Determining the Izod Pendulum Impact Resistance of Plastics.
- [3] ASTM International, ASTM D638 — Standard Test Method for Tensile Properties of Plastics.
- [4] International Organization for Standardization, ISO 21920-1:2021 — Geometrical product specifications (GPS) — Surface texture: Profile — Part 1.
- [5] International Organization for Standardization, ISO 6603-1 — Plastics — Determination of puncture impact behaviour of rigid plastics.
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.