
Buyers should approve metal insert molding only after the metal/plastic interface has a controlled definition, the functional risks have an agreed verification route, and the first-part acceptance evidence is specified. In practical terms, that means approving an insert revision and loading orientation, the resin grade and intended environment, the datums that govern fit, and the inspection method—not simply a 3D model or a sample image. The approval should remain conditional where pull-out, torque, conductivity, sealing, sterilisation, or another application-specific duty still needs testing.
The ISO product page identifies ISO 20457:2018 as withdrawn and points users to ISO 20457:2026; use the current controlled requirement, not an outdated default. [2]
01
Define the insert as a controlled functional component
Start with the insert itself. The controlled drawing or specification should identify its material designation, finish or coating, supplier-controlled part number where relevant, geometry revision, critical external features, and permitted burr or contamination condition. Also show which areas are intended to be encapsulated, exposed, sealed, or used as a locating reference. Insert molding generally places a preformed component—often metal—into the mold before plastic is molded around it; threaded inserts, bushings, and sleeves are common examples [1]. That simple process description does not define the functional interface for a particular part.
Ask what the molded polymer is meant to achieve: electrical isolation, retention, alignment, load transfer, abrasion resistance, or merely position holding. Then ask whether retention depends on geometry, plastic contact, a shoulder, or a separate assembly feature. A knurl, groove, flat, or head may be useful only if it corresponds to the part’s load case and can be filled and inspected as intended. Specify the insert’s orientation and allowable protrusion relative to functional datums. This prevents a nominally correct insert from being positioned incorrectly for the final assembly.

02
Choose a loading and tooling route before approving cost or timing
The buyer should request a proposed loading concept early: hand-loaded with mistake-proofing, fixture-loaded, automated, or a process such as vertical injection molding. The appropriate route is part-specific. It depends on insert geometry, magnetic behaviour, access for loading, operator safety, required orientation control, planned volume, and what happens if an insert is missing or doubles up. The important approval question is not whether one route is universally better; it is whether the chosen route has a credible way to establish presence, position, and repeatability for this design.
Tooling review should also identify how the insert is located, supported against injection force, and protected from damage during mold close and ejection. Request the assumed gate region, likely knit-line locations near the interface, venting approach, and any shut-offs that could affect flash or steel wear. Protolabs notes that draft helps ejection and that thick features can lead to sink or warp, illustrating why nearby plastic geometry belongs in this review [1]. These are engineering topics for the proposed part, not universal approval limits.
| Approval question | Evidence to accept | Hold point to resolve |
|---|---|---|
| Is the insert unambiguous? | Revision-controlled insert drawing, material/finish and orientation | Multiple insert variants or undefined exposed length |
| Can it be loaded reliably? | Location/support concept and an insert-presence response plan | Uncontrolled hand orientation or no missing-insert strategy |
| Will the interface stay functional? | Part-specific load, temperature and environment validation plan | Retention or electrical duty assumed from geometry alone |
| Can conformity be measured? | Datums, CTQs, fixtures and report format defined | Only overall dimensions are listed |
03
Review resin behaviour, loading and warpage as one interface risk
A metal insert and a polymer do not respond to heating, cooling, moisture exposure, assembly load, or service temperature in the same way. Buyers should therefore ask for the selected resin grade—not just a resin family—and the conditions the finished part is expected to see. Consider whether the interface must resist rotation, axial force, thermal cycling, vibration, chemicals, or electrical requirements. These are part-specific validation decisions; an approval review cannot convert general material information into a product claim or regulatory approval.
For complex geometry, make injection molding warpage a named review item rather than a late corrective action. Autodesk explains that molding simulation can be used to assess filling, sink marks, weld lines, and whether faces deform out of plane relative to a flatness tolerance [3]. A simulation is an input to design judgement, not proof of production performance. Request the assumptions behind any analysis—resin data, gate concept, geometry version, and acceptance criterion—and decide which predicted risks require first-article measurement or functional testing.
04
Approve CTQs and the measurement plan at the same time
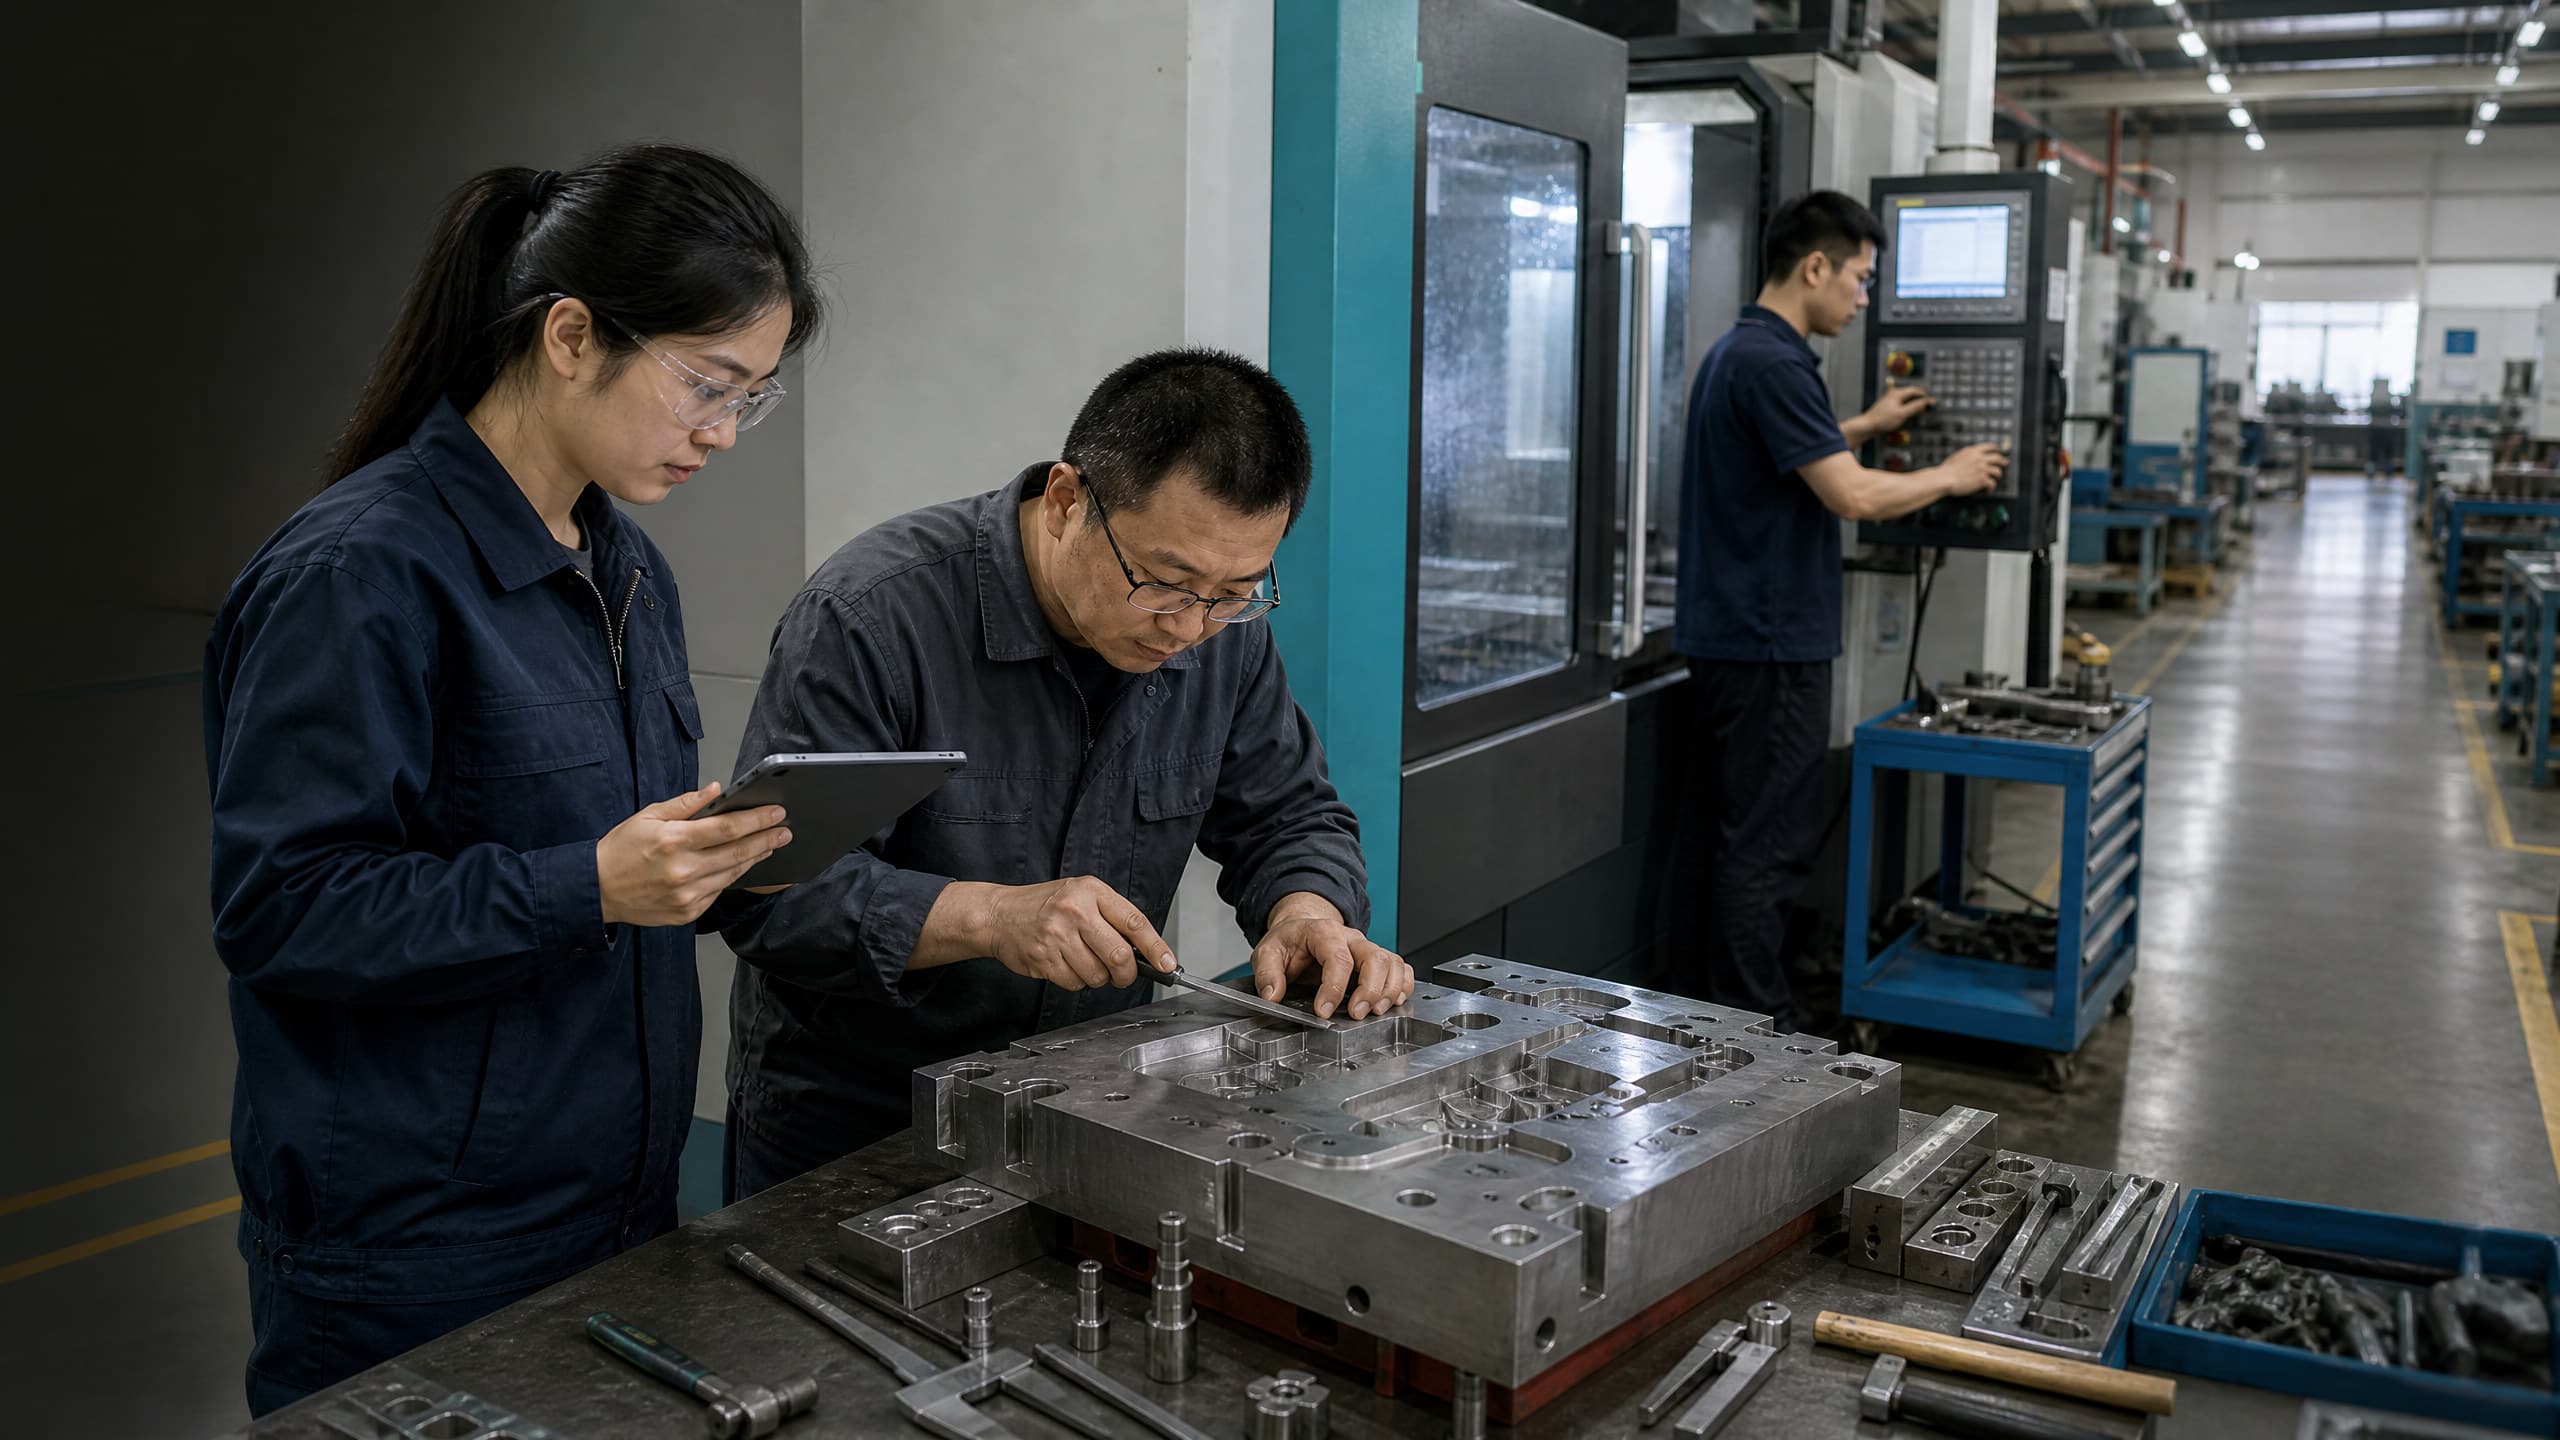
Create a short, interface-specific injection molding CTQ list. It might include insert height or depth from a datum, axis location, angular orientation, concentricity with a mating feature, exposed-thread condition, cosmetic flash at the metal edge, or an electrical continuity check where applicable. Tie each CTQ to the functional drawing datum and state the measurement method, fixture condition, sample basis, report units, and reaction when a result is outside agreement. Avoid applying a single tight tolerance to every plastic dimension; the most useful controls are the ones connected to assembly and use.
Plan injection molding inspection around the part’s real measurement challenge. ZEISS describes first-article work using a measurement plan, CAD model, or PMI/GD&T data, and identifies visual inspection, dimensional geometry, material thickness, warpage, shrinkage, and cavity comparison among applicable checks [4]. That does not prescribe a single method for every program. A CMM, optical system, dedicated functional gauge, cross-section, or visual standard should be selected because it can answer the agreed question. The ISO page says ISO 20457:2018 was withdrawn and replaced by ISO 20457:2026 [2]; confirm the applicable edition and any sector or customer requirements in the controlled agreement.
05
Make approval a documented release decision, not a sample impression
Before tool release or a production order, consolidate the decision into a buyer-readable approval pack: the controlled part and insert drawings; resin grade and colour specification; tooling and loading assumptions; CTQs and datum scheme; proposed first-article report; functional test plan where needed; cosmetic limits; packaging protections for exposed metal; and a change-notification route. Define who may approve deviations and what changes trigger review, such as a resin grade, insert source, coating, tool repair, gate change, fixture change, or measurement method. This gives procurement and engineering the same baseline when the project moves from quote to trial parts.
For a quote or engineering review, send the CAD and controlled drawings, insert data sheet or part number, intended load/environment, forecast quantity, and the five checks below. Ask the prospective insert molding service to identify assumptions and unresolved risks in writing. If the commercial discussion needs a clean hand-off, a buyer can request a document list and review scope through info@injeform.com. The outcome to seek is not a generic assurance; it is a part-specific agreement on what will be made, what will be measured, and what still requires validation.
Practical takeaway
Before you move
to the next review.
- Freeze the insert revision, material/finish, orientation, exposed length, and features that provide retention or location.
- Agree the loading, locating, support, presence-check, and response approach for a missing, damaged, or misoriented insert.
- Record the resin grade, intended service conditions, and part-specific validation needs for mechanical, electrical, sealing, or environmental duty.
- Mark interface CTQs and functional datums on the controlled drawing, then define the inspection fixture, method, report, and acceptance agreement.
- Approve a change-control list covering the insert, resin, tool, gate, loading method, inspection method, and packaging before placing the order.
FAQ
Common questions
Does metal insert molding automatically provide a pull-out or torque rating?
No. The process can integrate a preformed metal component with plastic, but a usable pull-out, torque, or rotation-resistance requirement comes from the part’s geometry, resin, insert design, molding conditions, service environment, and test method. Define the load direction, conditioning, fixture, pass/fail criterion, and reporting expectation for the particular application before treating a result as an approval basis.
Should buyers require simulation before approval?
Simulation can be useful when flow, weld lines, deformation, or gate choices could affect the interface. It is most valuable when the model, material data, boundary conditions, and decision it will inform are clear. Autodesk describes simulation as a way to investigate filling and warpage-related issues [3], but it should complement—not replace—first-article measurement and any functional validation required by the part.
What must be in a first-article report for an insert-molded part?
At minimum, agree in advance which interface dimensions, insert orientation or exposure features, visual conditions, and functional checks will be reported against which datums. Include the drawing revision, sample identification, measurement method, results, and any deviations. Add material, process, traceability, or regulatory records only when the application and contract require them; those obligations are not created by insert molding alone.
References
Source material
- [1] Protolabs, Design Guidelines: Overmolding & Insert Molding.
- [2] ISO, ISO 20457:2018 Plastics moulded parts — Tolerances and acceptance conditions (withdrawn; replaced by ISO 20457:2026).
- [3] Autodesk, What is Injection Molding Simulation in Autodesk Fusion?
- [4] ZEISS, First article inspection: Measuring technology for plastic parts.
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.