
Can design for assembly reduce the weight of an injection-molded product? It can, but the credible route is not simply to thin every wall. A team may remove duplicated flanges, shorten fasteners, consolidate compatible components, replace a bulky joint with an integrated snap or guided feature, or move material into a more effective load path. The result depends on resin, fiber loading, geometry, processing, environment, annual volume and the customer’s specifications. A lighter assembly can also introduce new joint loads, tolerance stack-up, local stress, impact sensitivity, warpage or serviceability risks.
For overseas OEM, procurement, quality, engineering and product teams, treat this as a product-architecture and sourcing decision. Freeze what the assembly must do, compare the baseline and proposed interfaces, and require evidence at each approval gate. Design for assembly is a recommendation framework; the released drawing, customer specification, safety obligations and validation plan remain the requirements.
Requirement: preserve approved function, interfaces, safety, appearance, service, environmental and compliance requirements unless their owner formally changes them. Recommendation: ask suppliers to show exactly where mass and assembly steps are removed, what new loads or tolerances are created, and which molded-part evidence closes each risk. Do not approve a lighter concept on a universal promise of lower cost, higher strength, shorter cycle time or compliance.
01
What should buyers define before combining weight reduction with design for assembly?
Document the baseline at assembly level, not only at part level. Record the approved part numbers and revisions, component and assembled mass measurement methods, part count, fastener and insert count, joining sequence, operator or automation assumptions, cycle or takt expectations, service steps, mating materials, critical datums, allowable deflection, drop and vibration cases, temperature and chemical exposure, and the annual-volume range. Identify whether the mass target applies to one molded component, the finished subassembly, packaging or the complete product.
Separate requirements from recommendations. Requirements include controlled interfaces, retention or sealing performance, electrical clearances, access, repair policy, appearance zones, customer-specific materials and defined acceptance tests. Recommendations may include an integrated boss, snap, living hinge, locating rib, captured nut, reduced flange or consolidated cover. A proposed feature is not automatically acceptable because it removes a separate component or fastener.
Ask each supplier for a baseline-versus-proposed assembly map and a marked-up CAD section. The response should identify removed parts, new molded features, changed load paths, tolerance-stack assumptions, tooling impact, expected mass change, assembly sequence, inspection changes and unresolved questions. This makes quotations comparable and helps the product owner decide whether a changed interface is a design improvement or an unapproved requirement change.

02
Which design-for-assembly routes may reduce molded weight without weakening the product boundary?
Start with the function of each feature. A flange that only locates a cover may be replaceable by a smaller datum-and-retention arrangement; a duplicated bracket may be consolidated if the new load path and service access are acceptable; a thick solid boss may be cored and supported with ribs or a locally revised fastening strategy. These are concepts to compare, not default rules. Stiffness, impact resistance, creep, assembly force and joint durability can move in different directions when material is removed or redirected.
A design-for-assembly change can transfer risk from component manufacture to the interface. A snap may reduce screws but introduce insertion-force variation, notch sensitivity, wear, repair limits or stress concentration. An integrated locator may reduce parts but make molding, ejection, measurement or replacement harder. A consolidated shell may reduce mass and part count but increase mold complexity, warpage sensitivity or the consequence of one rejected part. Review the whole assembly and intended service environment before selecting a route.
Use the following comparison as an RFQ discussion aid. The supplier should state assumptions for the actual resin, fiber loading, geometry, process, environment, volume and customer specification.
| Design-for-assembly route | Potential mass or assembly benefit | Evidence and approval question |
|---|---|---|
| Remove duplicated brackets, flanges or spacers | May reduce molded material and separate hardware when the same datum, retention and load function can be achieved once. | Does the new load path meet deflection, vibration, impact and service requirements? Has tolerance stack-up been recalculated? |
| Integrate locating, guiding or retention features | May reduce loose components, fasteners and manual operations. | Request insertion and retention-force data, wear or reuse assumptions, local stress review, draft/ejection review and a repair decision. |
| Core a bulky joint or boss and redesign the reinforcement | May remove local mass while preserving a fastening or locating function. | Review sink, voids, weld lines, cooling, warpage, pull direction, tool steel and the actual fastener or insert load. |
| Consolidate compatible molded components | May reduce part interfaces, hardware and assembly handling; mass may fall or may move into a more complex single part. | Confirm serviceability, inspection, tooling risk, cavity strategy, failure containment and whether one defect affects the whole subassembly. |
| Replace a joint with a controlled weld or molded interface | May remove hardware and overlapping material in suitable applications. | Define joint strength, leak or seal needs, process window, access, rework policy and environmental validation before release. |
03
How can teams protect stiffness, impact performance, shrinkage and warpage?
Weight reduction changes section geometry and therefore the relationship between material, load path and deflection. A ribbed or cored shape can be more efficient than a uniform thick wall, but rib orientation, junction radii, draft, weld lines and local transitions matter. For fiber-filled grades, orientation can make properties direction-sensitive; for unfilled grades, the balance of stiffness, toughness and creep may lead to a different choice. Compare the named resin grade and fiber loading in the intended geometry rather than relying on density or one datasheet value.
Material removal also changes filling, packing, cooling and shrinkage. New thin sections can challenge flow or joining; new thick-to-thin transitions can change local packing and sink; asymmetric ribs, bosses and integrated features can increase differential shrinkage and warpage. Gate location, venting, cooling, ejection and process window should be reviewed against the assembly datums and mating faces. Simulation can screen concepts, but molded parts under agreed conditions must close the decisions that affect release.
Require the supplier to distinguish analysis assumptions from measured evidence. Ask for the material designation, data source, fiber orientation assumptions where relevant, boundary conditions, load cases, predicted deflection, warpage and tolerance implications, plus the limitations of the model. Then agree which molded-part checks are required: mass, critical dimensions, assembly force, fit, retention, impact, vibration, environmental exposure or other product-specific tests. No universal weight saving or strength outcome should be inferred from a geometry rule.
04
What should procurement request before approving a lightweight assembly concept?
Request a controlled comparison package before tooling commitment: baseline and proposed CAD revisions, assembly tree, part and subassembly mass measured by an agreed method, removed and added features, named resin and reinforcement, process assumptions, tool concept, cavity or insert implications, preliminary tolerance stack, assembly sequence, quality risks, expected annual volume and a change-cost and schedule view. Ask whether the proposal requires new steel, mold modification, different equipment, fixtures, joining equipment, inspection gauges or new work instructions.
Require supplier evidence requests to be traceable to risks. For example, a snap proposal should identify insertion, retention, fatigue, temperature and reuse evidence; a consolidated shell should identify warpage, fit, appearance, service and containment evidence; a changed fastener boss should identify torque, pull-out, creep and assembly-angle evidence. The supplier should also state material lot identification, permitted substitutions, regrind or recycled-content assumptions, colour and finish controls, and how changes will be notified.
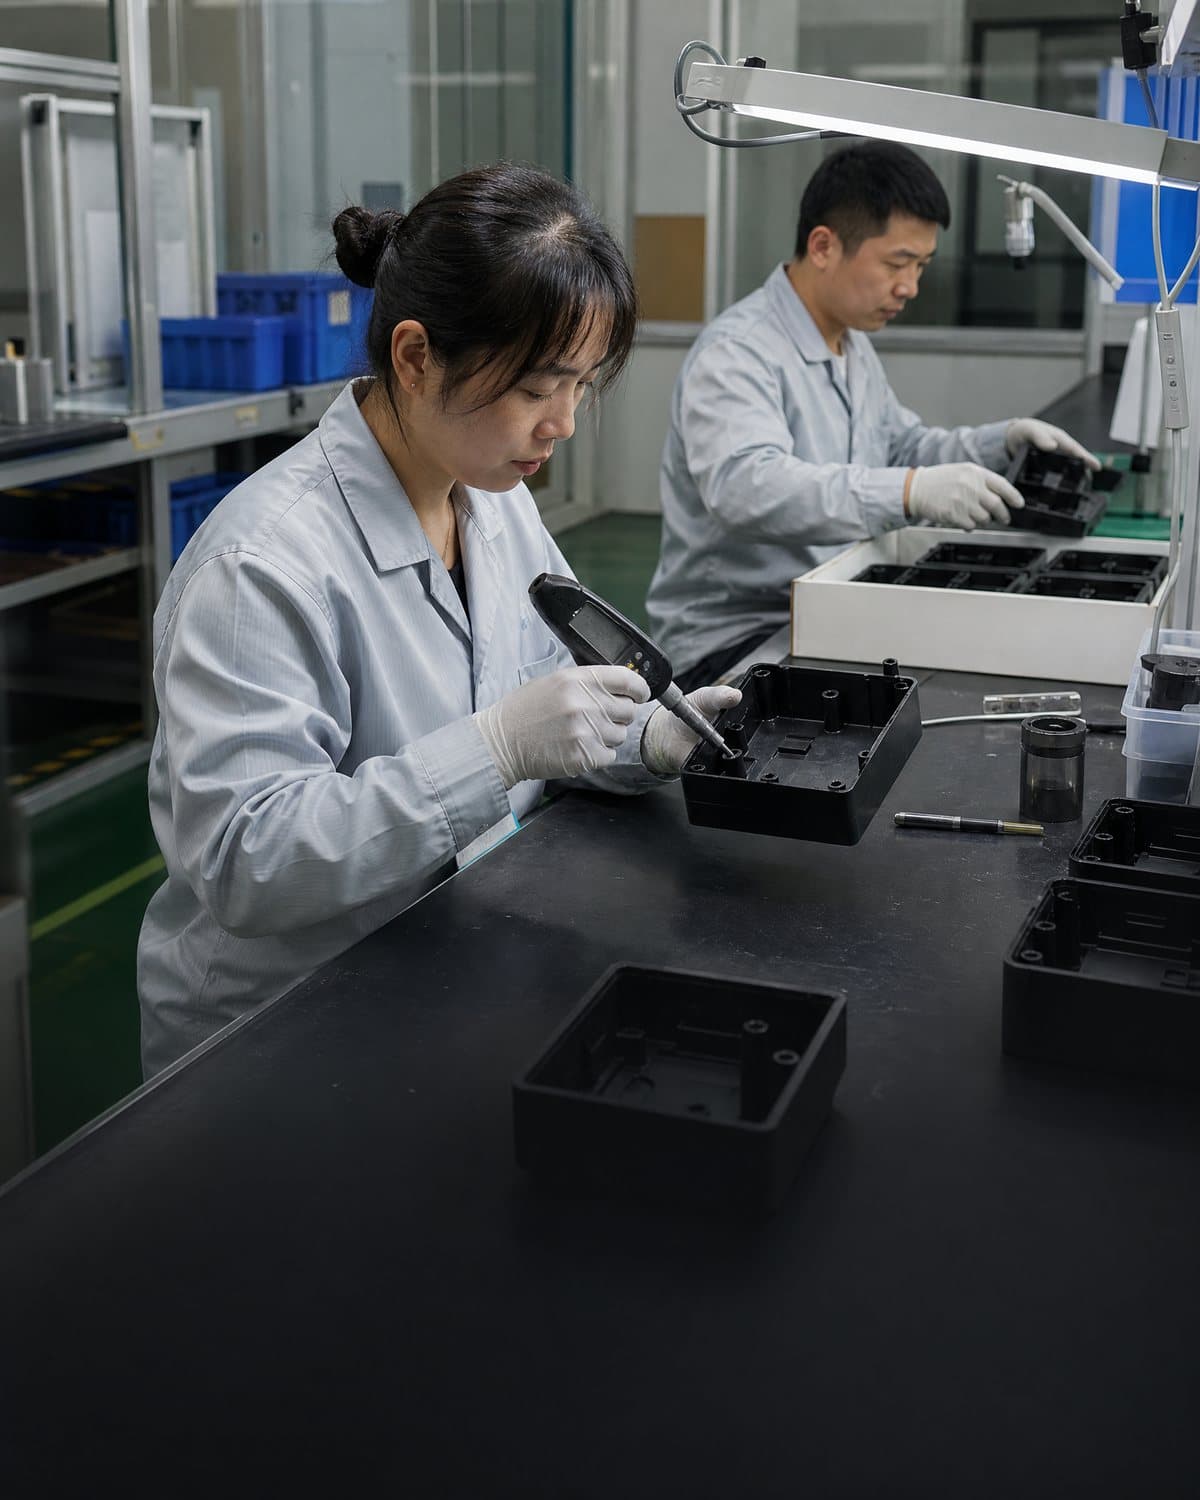
Do not treat a first-off sample, simulation report or calibrated measurement report as automatic product qualification. Quality and engineering should confirm the sample’s material, tool, cavity, process condition, conditioning state, measurement method, drawing revision and acceptance criteria. For regulated, safety-related, sealing, electrical or high-consequence products, the product owner must define the applicable validation and compliance route; a general molding recommendation cannot establish it.
05
Which approval gates keep a design-for-assembly weight change controlled?
Use staged gates with named owners. Gate 1 freezes the baseline, requirements, mass measurement method and non-negotiable interfaces. Gate 2 selects a concept after supplier DFM, load-path, material, tolerance and tooling review. Gate 3 approves the detailed CAD, drawing, named grade, joining method, inspection plan and validation matrix before steel release. Gate 4 reviews trial parts for mass, dimensions, fit, assembly sequence, appearance and any agreed functional or environmental tests. Gate 5 releases production only after open deviations, control-plan updates, change control, capacity and documentation are closed.
At every gate, distinguish a requirement from a recommendation and record the decision owner. Procurement may compare quoted tooling, piece price, labor and logistics; engineering owns functional feasibility; quality owns evidence and reaction planning; product or customer authority owns requirement changes. A supplier may propose a lighter architecture, but should not silently redefine a tolerance, material, service condition or compliance basis to make the target appear achievable.
A practical acceptance record should include the approved baseline and proposed revisions, part and assembly mass, named material, tool and cavity identification where applicable, critical dimensions and datums, assembly checks, test conditions, deviations, disposition, change-notification rules and the next review date. If the product later changes resin, fiber loading, gate, joining process, environment, volume or customer specification, reassess whether the original weight-reduction evidence still applies.

Practical takeaway
Before you move
to the next review.
- Freeze the baseline part and assembly revisions, mass measurement condition, part count, joining sequence and non-negotiable product requirements.
- Ask suppliers to show the removed and added features, revised load paths, tolerance stack, named resin or fiber loading, tooling impact and expected mass change.
- Review stiffness, impact, creep, shrinkage, warpage, assembly force, serviceability and environmental risks for the actual geometry and process.
- Define evidence by risk, including molded-part mass, critical dimensions, fit, retention or sealing, material traceability and product-specific functional tests.
- Use formal approval gates before tool release and production release, with named owners for engineering, quality, procurement, product and customer decisions.
FAQ
Common questions
Can design for assembly always reduce injection-molded product weight?
No. It may remove duplicated features, hardware or interfaces, but a consolidated part can require added ribs, local reinforcement or more complex tooling. The outcome depends on resin, fiber loading, geometry, process, environment, volume and customer requirements. Confirm the actual part and assembly mass by an agreed method.
Is a snap-fit automatically better than screws for a lightweight plastic assembly?
No. A snap-fit may reduce hardware and assembly steps, but it introduces insertion force, retention, fatigue, impact, creep, tolerance and serviceability questions. Specify the use cycle, temperature, mating materials and acceptance tests, then validate the molded feature in the intended geometry.
How does lightweighting affect warpage and dimensional fit?
Changing walls, ribs, bosses, gates or material can change flow orientation, packing, cooling and shrinkage. These effects may alter warpage or assembly datums, especially in asymmetric parts. Review the tool and process concept, then measure critical interfaces on molded parts under defined conditions.
What should an OEM require from a supplier before approving a lighter assembly?
Require controlled CAD and drawings, a baseline-versus-proposed mass comparison, named material and process assumptions, load-path and tolerance review, tooling impact, assembly-risk register, evidence plan, trial results and documented approval owners. A simulation or first-off sample alone does not prove production qualification.
References
Source material
- [1] Autodesk Moldflow Help: Runner balance analysis
- [2] ASTM D638: Standard Test Method for Tensile Properties of Plastics
- [3] ASTM D955: Standard Test Method for Mold Shrinkage of Plastics
- [4] ISO 20457: Plastics moulded parts — Tolerances and acceptance conditions
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.