
Improving a plastic part’s stiffness-to-weight ratio is not the same as simply removing material. A lighter injection-molded component may deflect more, lose impact margin, or become harder to mold consistently if the load path, resin, wall distribution and process window are not considered together. For overseas OEM, procurement, quality and engineering teams, the practical question is: can the part meet its defined stiffness and durability requirements at lower mass, with evidence that supports tooling release and production approval?
The answer depends on the resin grade, fiber loading, geometry, processing conditions, service temperature, moisture or chemical exposure, annual volume and customer specifications. Use the framework below to compare design routes, request supplier evidence and set approval gates without treating a material datasheet or a generic weight-saving percentage as a part guarantee.
A lighter part is acceptable only when the measured load case, impact requirement, dimensional behavior and production evidence remain within the approved specification.
01
What improves stiffness-to-weight ratio in an injection-molded part?
Stiffness is governed by both material modulus and geometry. The same resin can resist bending more effectively when material is placed farther from the neutral axis, such as in a well-positioned shell, rib or channel, rather than concentrated in a thick solid wall. This is why a geometry-led redesign can outperform simply increasing wall thickness. The result still depends on load direction, support conditions, rib continuity, local stress concentrations and the way the mold fills.
Treat requirements and recommendations separately. The requirement is the function: for example, a maximum deflection under a defined force at a stated temperature and support condition. A rib, gusset, cored boss or higher-modulus grade is a recommendation to investigate, not an automatic solution. Confirm the load case with the product team before changing the part, and identify whether impact, fatigue, creep, sealing or cosmetic appearance is also a release criterion.
A supplier review should map the primary load path, mounting points, fastener interfaces, weld-line risks and visible surfaces. Ask for a comparison of the baseline and proposed CAD, part mass, predicted deflection assumptions, nominal and local wall sections, gate strategy and any expected fiber-orientation effects. A simulation is useful for screening concepts, but physical samples from representative tooling remain necessary for acceptance.

02
Compare the main lightweighting routes before changing the resin
No single route is best for every application. A thin-wall redesign can reduce mass but may narrow the filling and packing window. Ribs and gussets can add section depth efficiently but may create sink, read-through, weld-line or ejection concerns. A fiber-reinforced grade can raise modulus in the fiber direction, while also increasing anisotropy, tool wear sensitivity and directional shrinkage. The right choice depends on the part’s load path and environment rather than on a headline material property.
Use the following as a screening matrix. It is not a performance ranking and does not replace a grade-specific design review or test plan.
The supplier should state what changes in tooling, processing, inspection and validation are expected for the selected route. Procurement should request the exact commercial grade, reinforcement content, color or additive package, data-sheet revision, approved alternatives and resin traceability plan before comparing quotes.
| Route | Potential benefit | Typical risk to investigate | Evidence to request |
|---|---|---|---|
| Redistribute wall material with ribs or channels | Raises section depth without making the whole wall solid | Sink, weld lines, draft, ejection and local stress concentration | DFM review, mold-flow assumptions, T1 section inspection and deflection test |
| Reduce nominal wall thickness | Can reduce mass and material volume | Short shot, lower impact margin, buckling, warpage and process sensitivity | Fill analysis, capability data at critical walls and functional samples |
| Select a higher-modulus or reinforced resin | May increase stiffness at similar geometry | Directional properties, moisture response, brittleness, surface appearance and tool wear | Named grade TDS, conditioning plan, orientation review and mechanical test results |
| Add local gussets or cored bosses | Supports mounts and concentrated loads | Sink, voids, thick sections and assembly interference | Feature detail, sectioned samples, CT or other agreed inspection and load test |
| Change support or attachment geometry | Can shorten the effective span or improve load transfer | New assembly loads, tolerance stack-up and service-access effects | Updated interface drawing, tolerance review and assembled-part validation |
03
Control stiffness, impact and dimensional risks together
Stiffness is only one part of structural performance. A higher-modulus formulation can be less tolerant of impact or low-temperature shock in a particular design, while a thin section can reduce energy absorption even when its static deflection looks acceptable. Creep can increase deflection over time under sustained load, especially as temperature rises. Define the required test speed, temperature, duration, fixture, load direction and failure or deflection limit instead of using the word “strong” as the acceptance criterion.
Lightweighting also changes molding behavior. Thin or uneven sections can alter filling, packing and cooling. Thick rib bases, bosses and transitions can cool more slowly and contribute to sink or void risk. Fiber-filled compounds can shrink differently parallel and perpendicular to flow, so gate position and flow direction may affect flatness and fit. Shrinkage data from a standard specimen should be treated as a design input, not as an absolute allowance for a complex production part.
The approval package should identify critical-to-quality dimensions, free-state versus assembled measurements, conditioning state, measurement timing and the disposition of any tool change. If a lighter design changes the gate, cavity steel, cooling layout or ejection scheme, treat that as a tooling and validation change—not only a CAD revision.
04
Make tooling and process choices part of the lightweighting decision
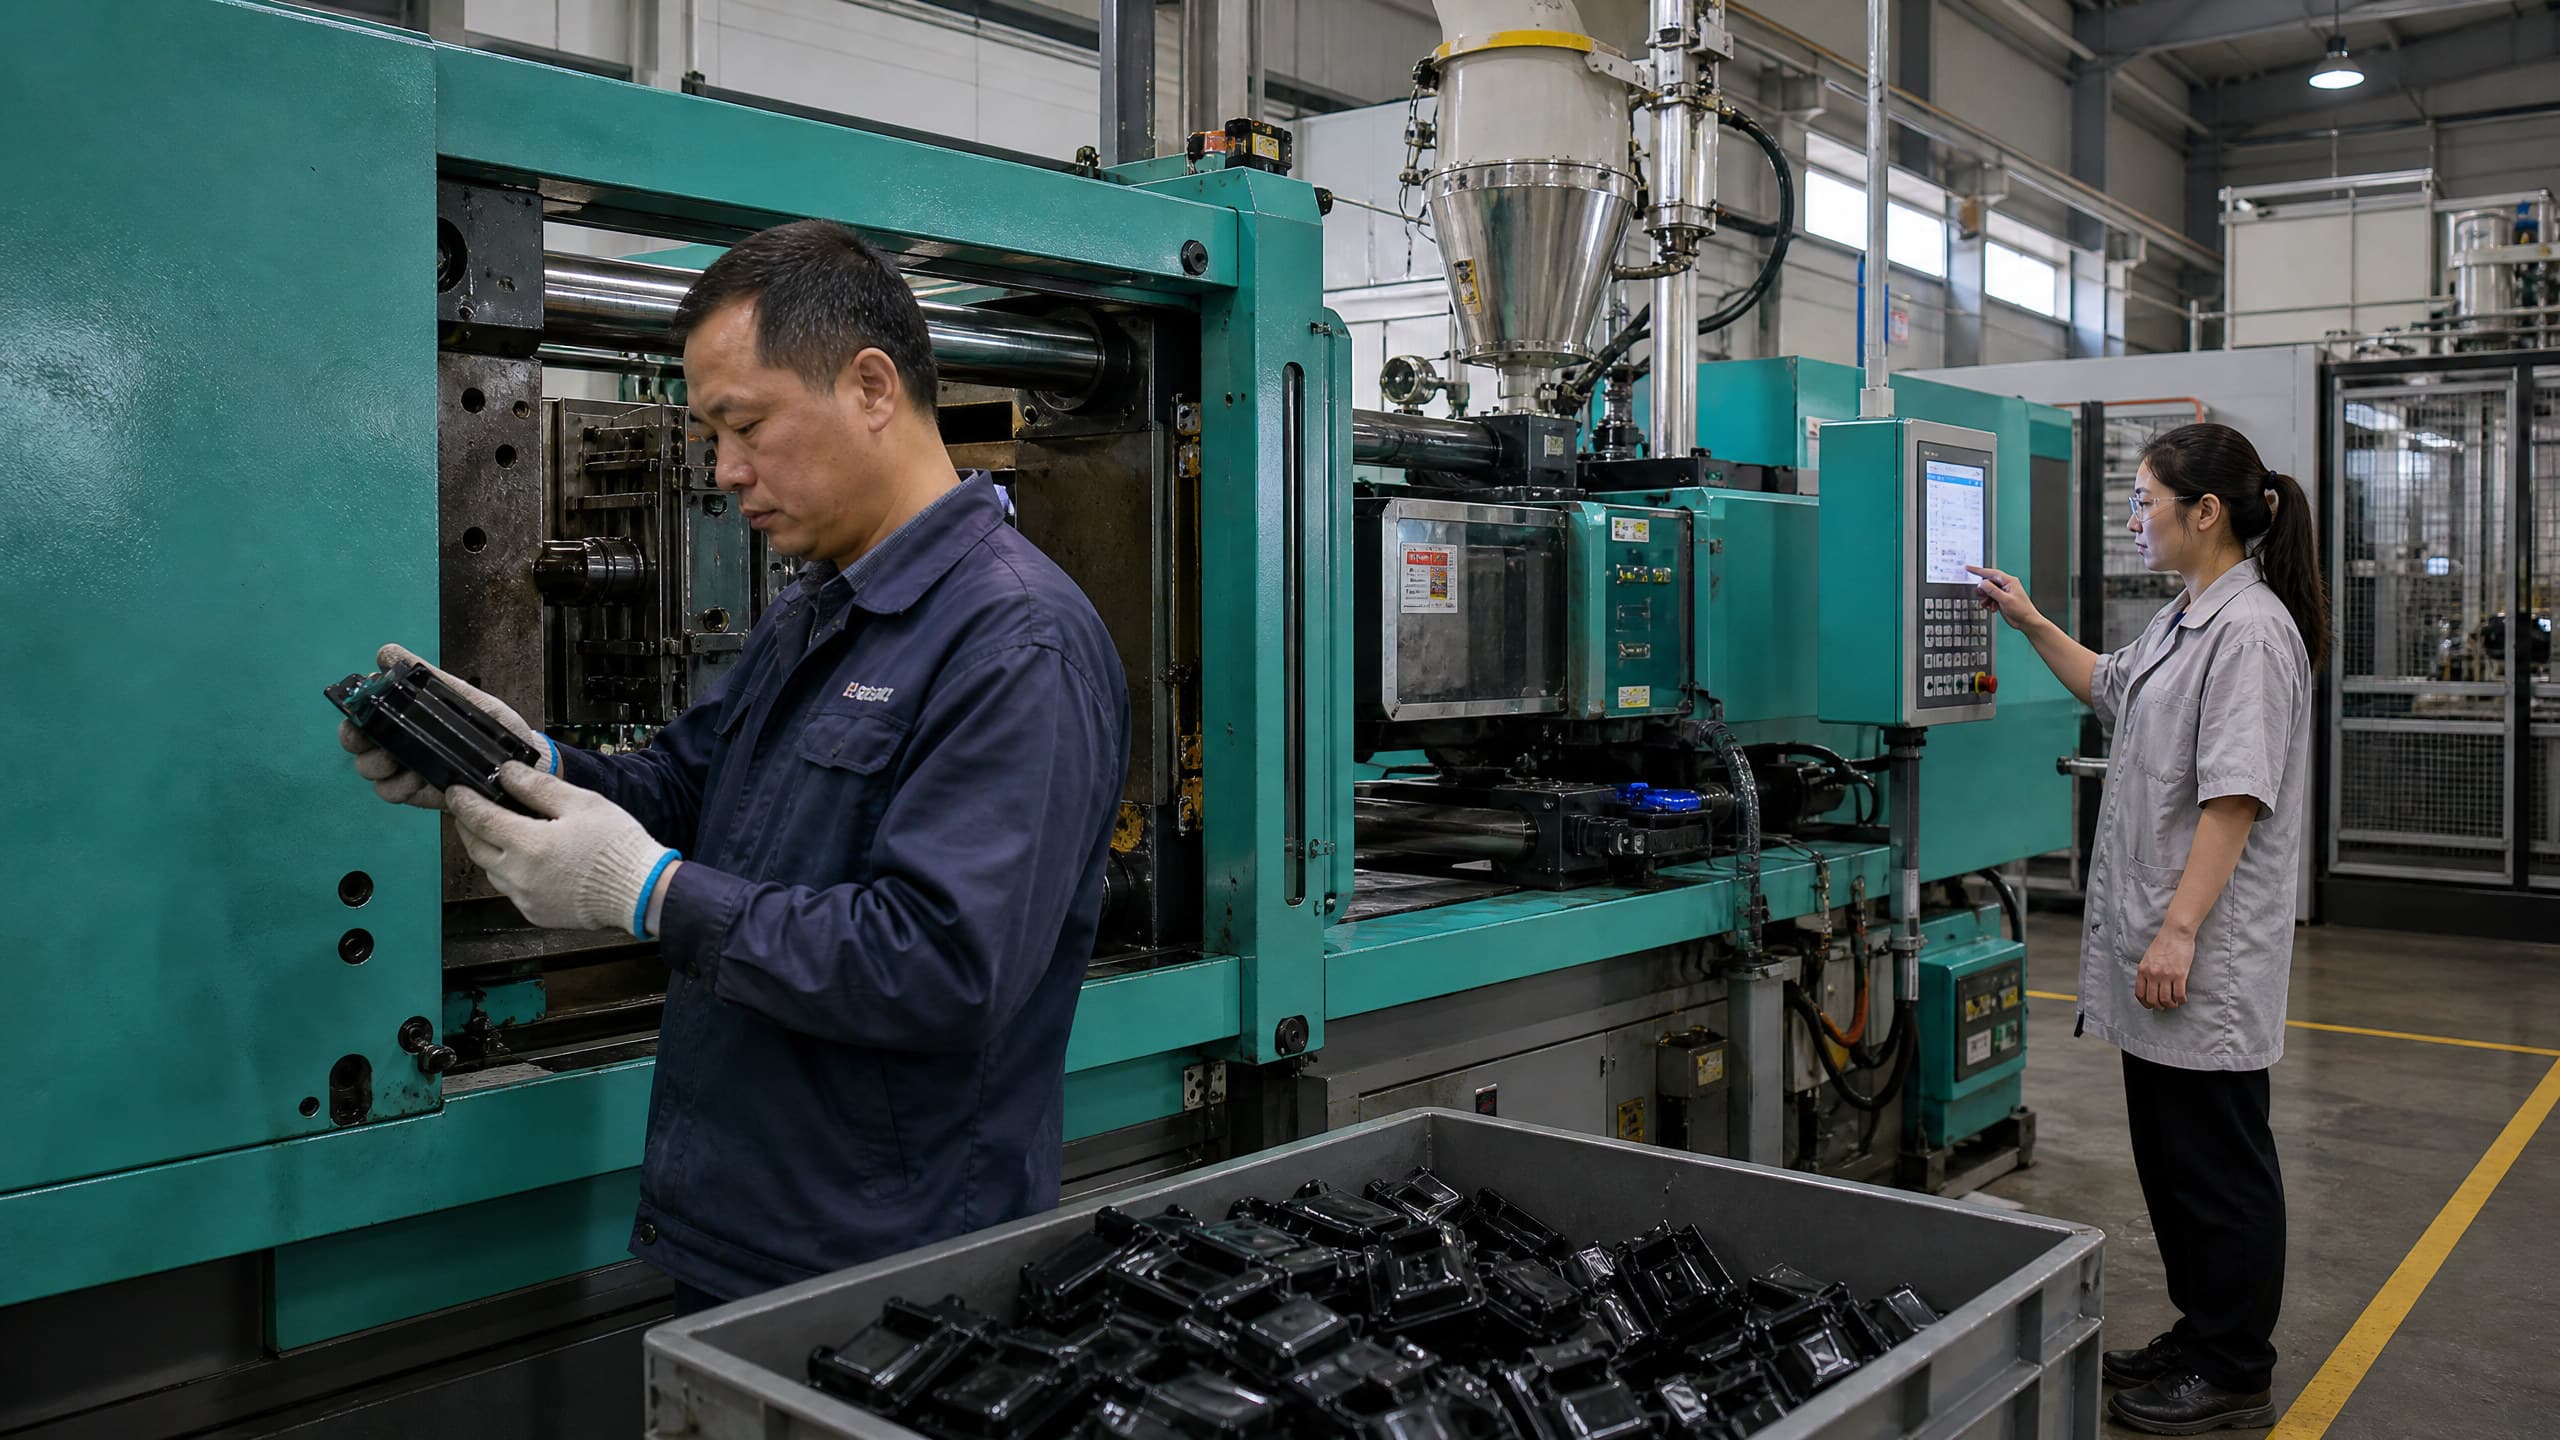
A stiffness-to-weight redesign should be reviewed before steel is cut. Confirm draft on ribs and gussets, shutoff feasibility, parting-line location, venting, gate and runner balance, cooling access, ejector support and likely weld-line locations. A geometry that looks efficient in CAD may require slides, lifters, additional inserts or a different gate arrangement. Those choices can affect tool cost, maintenance, cycle stability and cosmetic acceptance.
Ask the molder to document the proposed process window rather than quoting one machine setting as a universal recipe. The named resin’s drying or storage requirements, melt and mold temperature ranges, fill and pack profile, cooling balance and regrind controls should be linked to the actual part. If the part uses glass or mineral reinforcement, ask how fiber orientation, abrasion and cavity-to-cavity variation will be monitored.
For an overseas program, define evidence ownership in the RFQ. The supplier should identify who owns the mold-flow file, trial records, material certificates, dimensional report, functional test data, control plan and change history. Require an approval gate at design review, T1 or first-off samples, capability confirmation for CTQs and production release. Do not approve a lighter design solely because the quoted piece price or nominal part weight is lower.
05
Validate the finished part and release it with defined gates
A practical validation plan compares the baseline and lightweight design under the same defined conditions. Measure part mass and critical dimensions, then test stiffness or deflection using the real support and load interfaces where possible. Add impact, fatigue, creep, thermal cycling, humidity or chemical exposure when those conditions are credible in service. The test matrix should be agreed by engineering and quality before samples are molded.
Use production-intent resin, color and process settings for the release decision. Record cavity, resin lot, conditioning state, molding date and test fixture. For fiber-reinforced materials, consider whether samples represent the gate direction and flow history of the production cavity. A passing prototype made from a different grade, tool or process window should not be treated as production approval.
Recommended gates are: requirements freeze; DFM and simulation review; material and grade approval; tool trial review; first-article dimensional and visual approval; functional and environmental validation; process-capability review for CTQs; and documented production release. Acceptance limits, sample quantities, re-test rules, deviation authority and change-notification requirements should be written before the supplier starts the validation run.

Practical takeaway
Before you move
to the next review.
- Define the required stiffness, maximum deflection, impact, fatigue or creep limits with load, fixture, temperature, duration and conditioning state.
- Compare baseline and lightweight CAD for load paths, nominal and local walls, ribs, bosses, draft, interfaces, part mass and cosmetic zones.
- Approve the exact resin grade, reinforcement or additive package, color route, data-sheet revision, drying controls and permitted substitutions.
- Request supplier evidence covering mold-flow or equivalent DFM analysis, gate and cooling rationale, trial records, CTQ inspection and functional testing.
- Set release gates for tool changes, first articles, capability, environmental validation, deviations and engineering-change notification before production approval.
FAQ
Common questions
What is the fastest way to improve a plastic part’s stiffness-to-weight ratio?
Start with the load path and geometry, not a universal weight-saving target. Ribs, channels, gussets or improved attachment support may increase section efficiency, but their suitability depends on load direction, wall thickness, resin, molding feasibility, impact needs and appearance. Confirm the change with simulation and representative molded-part testing.
Does glass-filled plastic always provide the best lightweight injection-molding solution?
No. Glass reinforcement may increase modulus in some directions, but it can also create anisotropic shrinkage, moisture or temperature sensitivity, weld-line concerns, surface changes and additional tool wear. Select the named grade against the actual load, environment, geometry and customer specification, then validate the production-intent part.
Can thinner walls reduce cost as well as part weight?
Possibly, but it is not guaranteed. Less material may reduce mass, while thin walls can require higher filling pressure, tighter process control, different gates or longer development work. A supplier should show how the proposed wall change affects fill, pack, cooling, cycle stability, scrap risk and the quoted total cost at the expected volume.
What evidence should an OEM request before approving a lightweight injection-molded part?
Request the exact material and lot information, baseline-versus-new CAD and mass comparison, DFM or flow review, tooling and gate rationale, dimensional report, functional deflection or stiffness data, relevant impact or environmental results, process-capability evidence for CTQs and a documented change or deviation record. Samples should use production-intent tooling, resin and process conditions.
References
Source material
- [1] ASTM International, ASTM D638-22: Standard Test Method for Tensile Properties of Plastics
- [2] International Organization for Standardization, ISO 294-4:2018 Plastics — Injection moulding of test specimens — Part 4: Determination of moulding shrinkage
- [3] ASTM International, ASTM D955-21: Standard Test Method of Measuring Shrinkage from Mold Dimensions of Thermoplastics
- [4] U.S. Department of Energy, Materials Selection and Design for Lightweighting guidance
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.