
Short-glass-fiber-reinforced thermoplastics can help an OEM pursue lower mass while retaining useful stiffness in an injection-molded component. They are not a universal lightweighting solution: fiber loading, base resin, geometry, flow direction, processing, service environment, production volume and customer specifications all affect the result. For procurement and engineering teams, the decision is not simply whether a resin contains glass fiber. It is whether a named grade, molded in the proposed geometry and process, can meet the required load, dimensional, cosmetic, environmental and commercial objectives with acceptable evidence.
Treat short-glass-fiber material selection as a controlled design change. Require a named grade, stated fiber content, material documentation, DFM review, representative molded samples and an approval gate before releasing the lightweight concept to production tooling.
01
What short-glass-fiber plastic changes in a lightweight part
Short glass fibers are mixed into a thermoplastic matrix to alter the balance of stiffness, strength, dimensional movement and processing behavior. A filled grade may support a thinner or more structurally efficient design, but the practical mass outcome depends on how much material the geometry still needs for ribs, bosses, interfaces, draft, impact resistance and manufacturing robustness. A datasheet tensile or flexural value is not proof that a molded part will perform equally in every direction.
Fiber orientation follows the melt-flow pattern to some degree. This can make properties direction-dependent and can influence shrinkage, warpage, surface appearance, weld-line behavior and fastening performance. A rib that aligns with flow may respond differently from a transverse feature or a region near a weld line. Requirements should therefore identify the load path, critical interfaces, impact direction, temperature and environmental exposure. Recommendations such as adding fiber or reducing wall thickness should remain conditional until the actual geometry and process are reviewed.
Lightweighting may change more than mass. Stiffness can improve in a preferred direction while impact toughness, surface quality, weld-line strength, creep response or dimensional stability may require separate checks. The outcome also depends on resin family, fiber percentage, additive package, moisture condition, melt and mold temperatures, gate and cooling design, packing, machine capability and part conditioning. No universal percentage weight saving, strength improvement or cycle-time reduction should be assumed.

02
How buyers should compare grades and design routes
Start with the product requirement, not a generic label such as glass-filled nylon or reinforced polypropylene. The product owner should define the approved base-resin family or qualification path, required fiber loading or acceptable range, service temperature, impact demand, chemical and moisture exposure, electrical needs, appearance, joining method, recycled-content direction and end-of-life constraints where applicable. The supplier should then identify the exact producer, commercial grade, reinforcement state, colour or additive system, technical-data-sheet revision and any proposed alternative.
A lower-density material is not automatically the best route. Compare a material-only change with geometry changes such as coring, rib optimization, local bosses, load-path refinement or consolidation of components. A geometric route may reduce mass without introducing fiber-orientation sensitivity, while a filled grade may offer stiffness in a compact package but require more attention to anisotropy, abrasive wear, surface finish or tool maintenance. The right choice is application-specific and should be judged against the released function and evidence plan.
Use the following as an early screening map, not as an approval table. The grade, formulation and part-level result must be verified against the customer specification and representative molded articles.
The quote should separate material assumptions from tooling and production assumptions. Ask whether the proposed grade changes shrinkage data, gate or runner design, venting, cooling, drying, ejection, steel choice, cavity balance, inspection method or approved process window. If the supplier proposes an alternative grade, require a documented equivalence review rather than accepting a polymer-family substitution by email.
| Decision area | What to compare | Evidence or buyer action |
|---|---|---|
| Stiffness and load path | Directional modulus, rib and boss behavior, mounting loads and deflection at service temperature. | Request grade data plus part-level deflection or load testing in representative flow directions. |
| Impact and durability | Notched impact, fatigue, creep, snap or fastener loads and expected conditioning. | Define the failure mode and test temperature; do not infer durability from stiffness alone. |
| Dimensional behavior | Flow/transverse shrinkage, fiber orientation, warpage, tolerance stack and mating interfaces. | Require a shrinkage and warpage risk review linked to CAD features and inspection datums. |
| Processing and tooling | Drying where applicable, melt condition, abrasive wear, gates, vents, cooling and ejection. | Ask for a process and tool-impact statement before steel release. |
| Appearance and joining | Fiber read-through, gloss, weld lines, paint or plating compatibility, welding and inserts. | Approve a representative surface sample and joining method, not only a resin plaque. |
| Commercial and supply | Grade availability, colour control, lot traceability, volume, approved alternatives and change notice. | Align purchasing specification, source strategy and material-change approval rules. |
03
Design and tooling implications: stiffness is not free of trade-offs
A thinner wall can reduce mass, but it can also increase sensitivity to filling, pressure, cooling variation, short shots, sink, weld lines and local deflection. A rib can improve section efficiency, but its root and nearby show surface may create a thickness transition that affects sink or warpage. A filled resin can change the preferred gate location and the magnitude or direction of shrinkage. Review nominal walls, ribs, bosses, clips, inserts, holes and cosmetic faces together rather than applying one wall rule to the entire part.
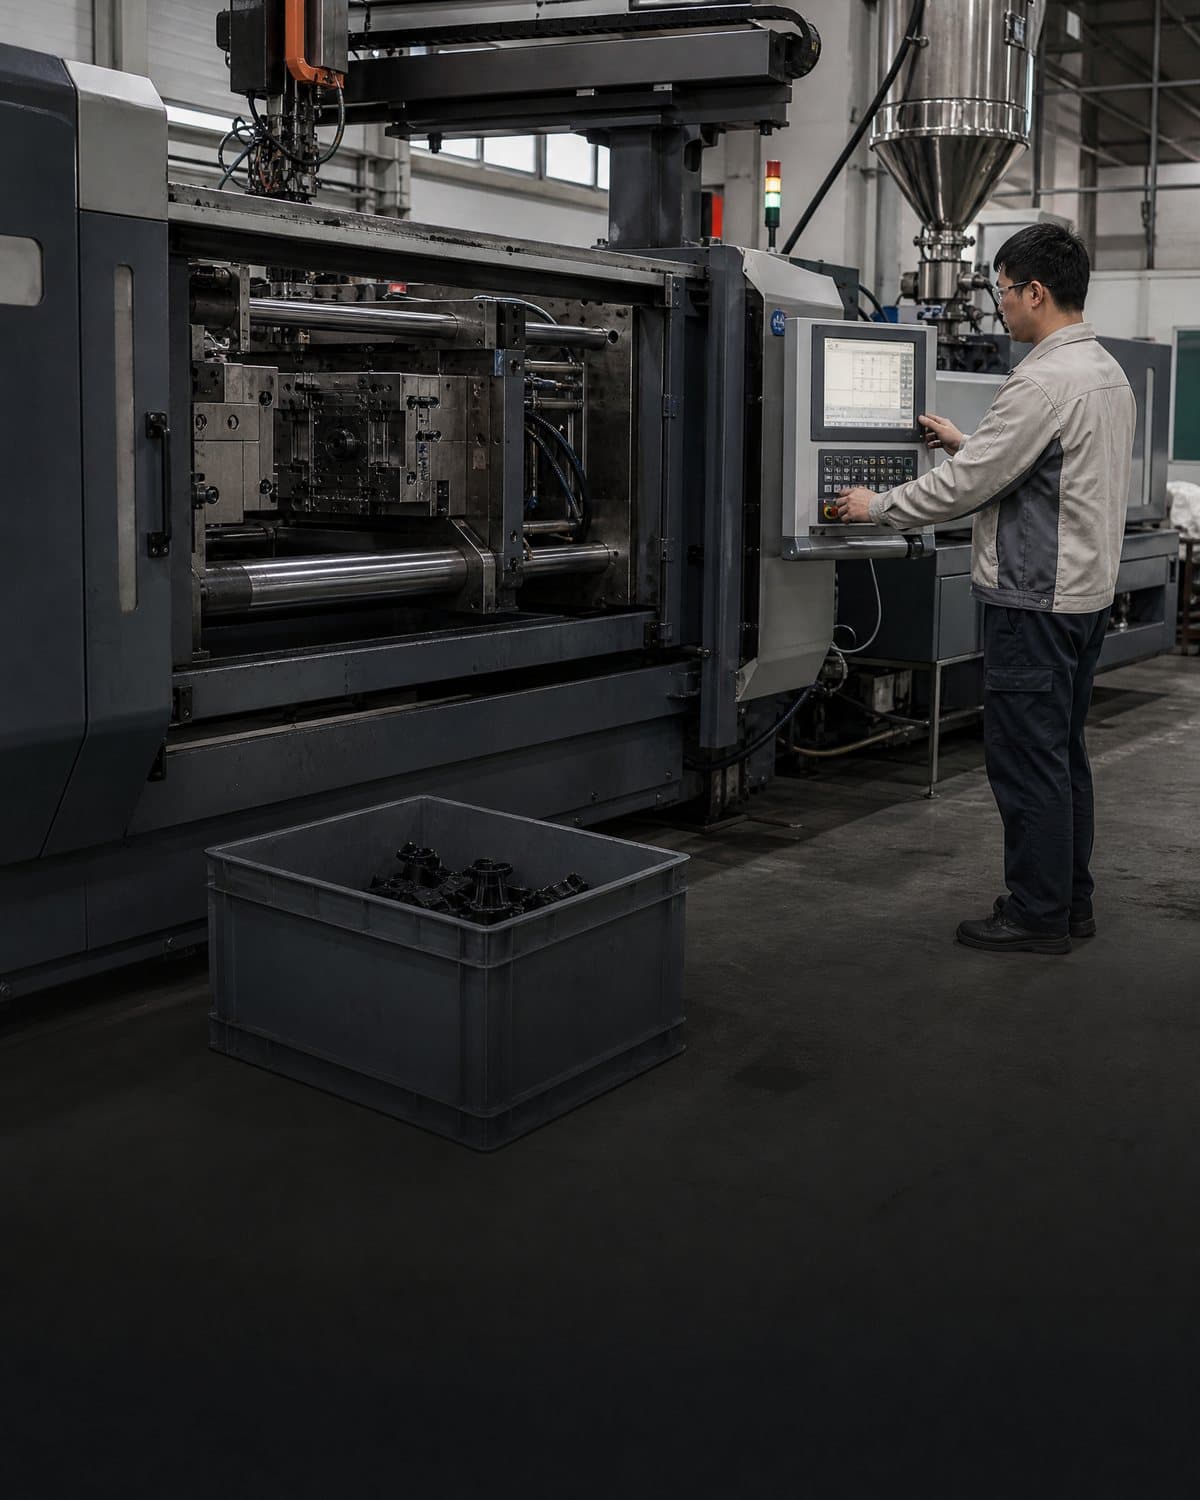
Tooling decisions should be made before the lightweight concept is treated as frozen. Ask the supplier to show the proposed parting line, gates, weld-line locations, vents, ejection, cooling strategy and any expected orientation-sensitive zones. Abrasive reinforcement may affect tool-material or maintenance considerations, depending on the grade and production plan. The supplier should also state whether the proposed change requires steel modification, new inserts, a different machine capacity, revised fixtures or a new inspection method.
Warpage is a system result, not a single material property. Non-uniform cooling, local thickness, fiber orientation, packing, tool temperature, cavity balance and restraint from inserts or assembly features can all matter. Simulation can help compare assumptions, but its usefulness depends on the selected material data, mesh, process inputs and geometry. Treat simulation output as a review input and risk map, not a production guarantee.
04
Validation plan for an OEM lightweighting decision
The minimum requirement is a documented approval plan that connects the claimed benefit to the product’s actual acceptance criteria. Freeze the baseline part revision, current material and mass-measurement condition, proposed grade, target environment, critical dimensions, load cases, cosmetic limits and customer approval authority before comparing results. A supplier recommendation is not a substitute for the product owner’s requirements.
Use production-intent or otherwise representative molded samples for decisions that depend on flow, orientation, shrinkage, cooling, weld lines, surface appearance, moisture or conditioning. Record cavity, machine, material lot, grade, colour, drying or conditioning, key process settings, sample quantity and inspection method. Compare baseline and lightweight versions using the same measurement definition. If the design changes the load path or assembly, repeat the relevant fit, functional, impact, thermal, chemical, fatigue, creep or joining tests rather than relying on an old approval.
Recommended approval gates are: material and supplier evidence review; DFM and tooling-risk review; first molded sample dimensional and visual review; functional and environmental validation; and production-process capability or control-plan approval as required by the customer. The required tests and acceptance limits vary by application. A first-shot part can demonstrate learning without proving all future lots, cavities or process settings.
Ask the supplier to report failed criteria and open assumptions, not only successful results. Evidence should include the exact grade, current documentation, relevant test conditions, any material substitution rule, process-change notification approach and corrective-action ownership. This creates an auditable purchasing decision and reduces the risk that an attractive part mass is approved without equivalent product performance.
05
Practical sourcing questions before approving the quotation
Procurement should ask for a like-for-like quotation that separates tooling, part price, material, inspection, testing, packaging and any secondary operations. Confirm the forecast by programme phase, expected tool life, cavity strategy, colour or grade availability, lead-time assumptions and logistics scope. A lower quoted unit cost may reflect a different grade, cavity count, inspection level, yield assumption or validation boundary.
Engineering and quality should require a marked-up DFM response. It should identify the material and fiber assumptions, predicted flow direction, high-risk interfaces, likely warpage zones, shrinkage basis, gate and ejection concept, and any design changes needed to make the part robust. Ask which items are requirements and which are recommendations. Require written customer approval for deviations to material, geometry, tooling concept or validation scope.
Do not accept unsupported claims such as guaranteed weight reduction, universal strength improvement, zero warpage, automatic compliance or a fixed cycle-time benefit. The credible supplier response will state dependencies and propose a controlled trial. InjeForm’s role in the sourcing discussion should be to clarify manufacturability and evidence needs; the OEM remains responsible for product requirements, qualification decisions and any market-specific compliance determination.

Practical takeaway
Before you move
to the next review.
- Freeze the baseline mass, CAD revision, material condition, critical interfaces and service environment before comparing lightweight options.
- Request the exact resin producer, commercial grade, glass-fiber content, additive or colour system, data-sheet revision and approved-alternative rule.
- Require a marked DFM review covering orientation, shrinkage, warpage, ribs, bosses, gates, cooling, ejection, tooling wear and inspection datums.
- Validate representative molded samples for the actual load, impact, temperature, moisture, chemical, cosmetic, assembly and dimensional risks.
- Set approval gates for material, DFM, tooling trial, functional validation and production control; record customer-approved deviations and changes.
FAQ
Common questions
Do short-glass-fiber plastics always make injection-molded parts lighter?
No. They can enable a more stiffness-efficient design in some applications, but mass depends on the full geometry, fiber loading, base resin, load path, wall sections, tooling and required robustness. A filled grade may also require local material or geometry changes. Compare the complete molded part against the baseline rather than assuming a universal weight saving.
What is the main risk of using short-glass-fiber plastic for a thin part?
A thin part can become more sensitive to directional stiffness, flow length, weld lines, filling and cooling variation. Fiber orientation may produce anisotropic shrinkage and warpage, while reduced section thickness can affect impact or assembly durability. Review the proposed geometry and process with representative molded samples before approval.
Should procurement specify a glass-fiber percentage or a named grade?
A named grade is normally the more actionable requirement because it identifies the resin family, formulation and documented properties. Fiber percentage is still relevant, but it does not define the entire material behavior. State the approved grade, required properties, substitution rules, traceability and customer-change approval process.
What supplier evidence should an OEM request before releasing tooling?
Request current material documentation, the exact grade and fiber state, processing and drying guidance where applicable, a CAD-linked DFM review, shrinkage and warpage assumptions, gate and cooling concept, tooling implications, sample and inspection plan, and a validation matrix tied to product requirements. Require written approval for material, geometry or process deviations.
References
Source material
- [1] ISO 294-1: Plastics — Injection moulding of test specimens — Part 1: General principles and moulding of multipurpose and bar test specimens
- [2] ISO 294-4: Plastics — Injection moulding of test specimens — Part 4: Determination of moulding shrinkage
- [3] ASTM D790: Standard Test Methods for Flexural Properties of Unreinforced and Reinforced Plastics and Electrical Insulating Materials
- [4] ASTM D638: Standard Test Method for Tensile Properties of Plastics
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.