
Lightweighting an injection molded part is not simply removing plastic from the CAD model. A thinner wall, a ribbed structure, a foamed or filled resin, or a redesigned load path can change stiffness, impact behavior, filling, packing, cooling, shrinkage, warpage, tooling and inspection. For an overseas OEM, the right question is whether the proposed mass reduction still meets the released functional requirements under the specified environment and production route. That answer depends on resin grade, fiber loading, geometry, processing, environment, volume and customer specifications.
Use this guide to turn a weight-reduction concept into a controlled sourcing decision. Treat every numerical target, resin substitution and geometry change as a requirement to be confirmed or a recommendation to be evaluated—not as a universal manufacturing promise.
A lighter part is successful only when its approved stiffness, impact, dimensional, assembly and environmental requirements remain satisfied. Ask the supplier to show what changed, what was tested, and which assumptions still require customer approval.
01
What changes when an injection molded part is made lighter?
Material removal usually lowers bending stiffness faster than it lowers mass because stiffness is strongly affected by section depth and the distribution of material around the neutral axis. A thin flat wall may weigh less but deflect more; a ribbed or locally contoured structure may preserve stiffness with less mass, although ribs can introduce sink, weld lines, local cooling differences and flow-orientation effects. Impact performance can also change with wall thickness, notch sensitivity, temperature, strain rate and resin toughness. Do not approve lightweighting from static stiffness alone.
The requirement is the product function: load, deflection, impact, fatigue, sealing, vibration, appearance, assembly and service temperature should be identified by the product team. A recommendation is the geometry or material route proposed to meet those requirements. Compare the baseline and lightweight concepts using the same boundary conditions, material state, conditioning and test method. Weight reduction, cost reduction or cycle-time improvement may occur, but none should be promised before representative evidence is available.
A lightweight design also changes procurement exposure. A higher-flow grade may fill a thin section but have different shrinkage or impact behavior. A glass-filled grade may increase stiffness but make anisotropic shrinkage and fiber orientation more important. Foamed or recycled systems may require their own qualification. Request the exact resin manufacturer, grade, colorant, additive and filler or recycled-content condition in the RFQ; a polymer family name is not enough.

02
How do design choices control shrinkage and warpage?
Shrinkage is the dimensional change as the molded material cools and, for some materials and geometries, continues to stabilize after ejection. Warpage is a shape deviation caused by unequal shrinkage and residual stress. Autodesk identifies non-uniform cooling, material variation, packing variation and machine variation as contributors to warpage [1]. BASF also links warpage to different packing, wall thickness, cooling, material behavior and fiber orientation [2]. Published shrinkage data is therefore a design input, not a guarantee of the finished dimension.
The primary recommendation is to keep wall sections as uniform as the function allows, transition thickness gradually, and use ribs or contours instead of isolated heavy sections. Ribs should be sized and located with sink, flow, ejection and load requirements in view; a common rule of thumb is not an acceptance criterion for every resin. Gate location and flow direction should be reviewed against visible faces, weld lines, long dimensions and fiber orientation. Cooling circuits, venting, packing and ejection must be assessed together because improving one variable can move the distortion elsewhere.
For a fiber-filled lightweight part, require an orientation and warpage review rather than assuming fibers only add stiffness. Fiber alignment can make shrinkage directional, especially around gates, weld lines, corners and flow turns. For unfilled or low-warpage alternatives, the trade-off may be lower modulus, different impact performance or a different temperature capability. The supplier should state which result is simulated, which is measured and which remains an assumption.
| Lightweighting lever | Potential benefit | Main shrinkage/warpage or performance risk | Evidence to request |
|---|---|---|---|
| Reduce nominal wall | Lower mass and possibly shorter heat-removal distance | Deflection, impact loss, short shot, pressure demand and sensitivity to variation | Flow/pack study, thickness map, stiffness and impact results on representative parts |
| Add ribs or local contours | Higher section efficiency without filling the whole volume | Sink, weld lines, local cooling imbalance, ejection marks and stress concentration | Rib DFM review, cosmetic map, warpage prediction and sectioned or measured samples |
| Use mineral- or glass-filled resin | Potentially higher modulus or dimensional stability in a chosen direction | Anisotropic shrinkage, fiber orientation, abrasive tooling wear and changed impact behavior | Exact grade data, orientation/warpage analysis, material traceability and mechanical tests |
| Change gate or cooling layout | More balanced filling, packing and thermal conditions | New vestige, weld-line, pressure, cycle or tool-maintenance trade-offs | Marked tool concept, simulation assumptions, trial settings and cavity-by-cavity results |
03
What should an OEM require from tooling and process planning?
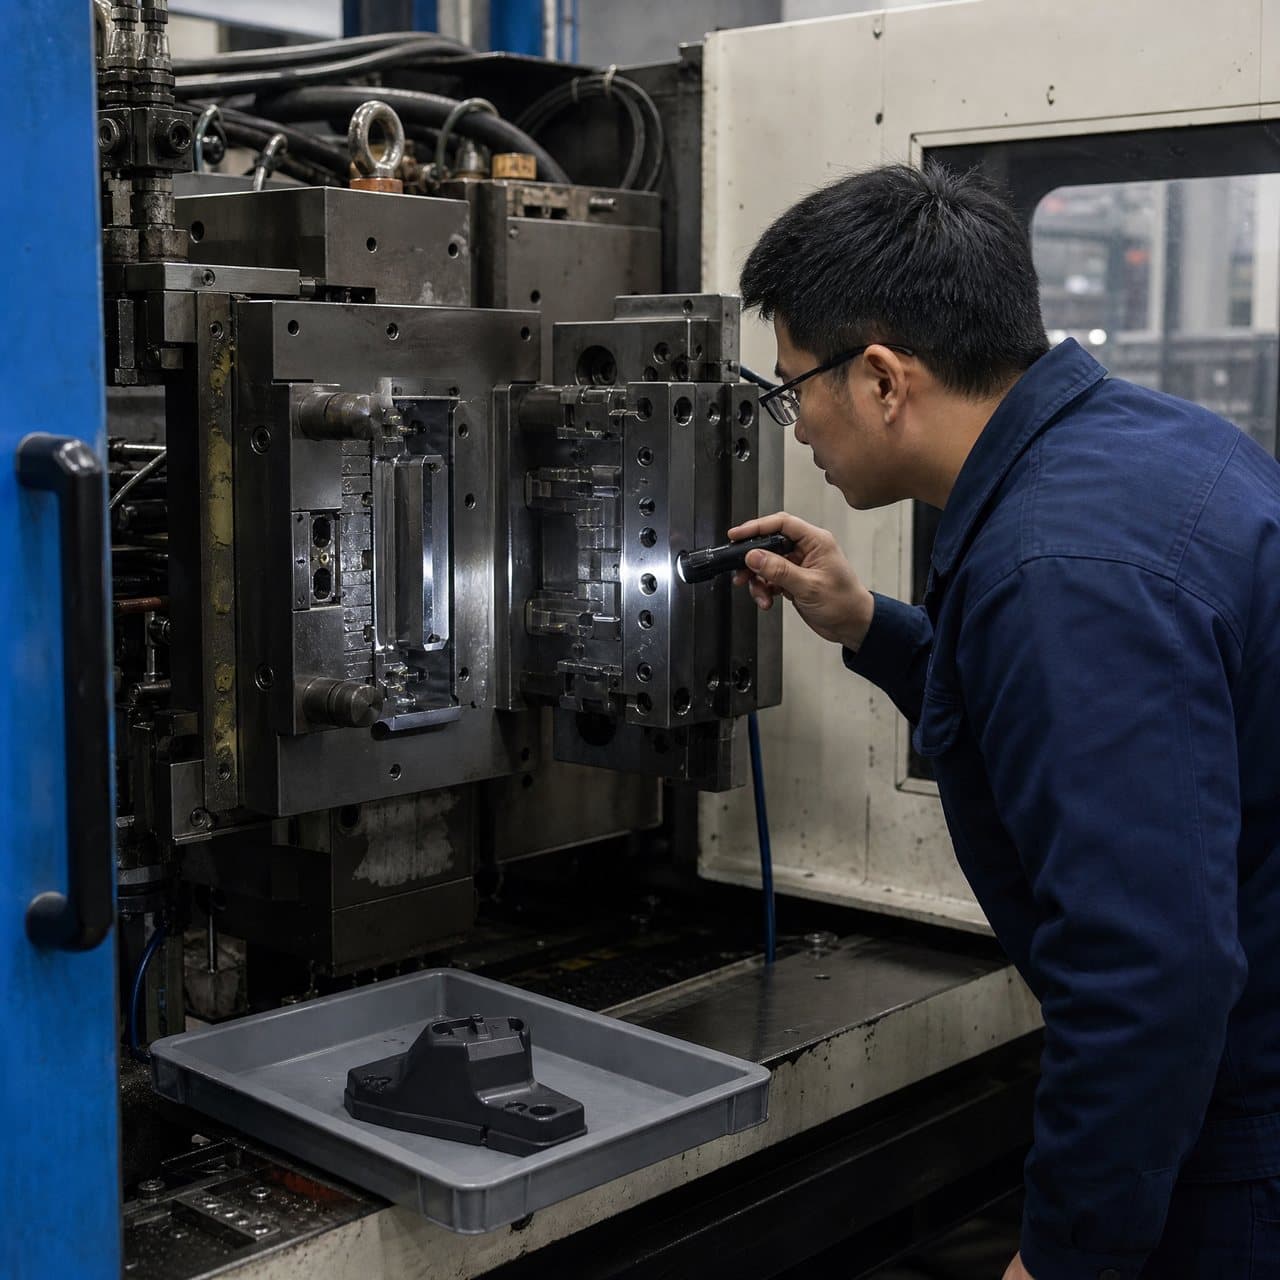
Before steel release, require a revision-controlled DFM response that marks nominal wall changes, ribs, bosses, datums, gates, vents, parting lines, ejection points, cooling strategy and any areas likely to distort. The supplier should identify must-change issues separately from recommendations. A tool can compensate expected material movement, but cavity compensation does not remove production variation or measurement uncertainty.
Ask for a mold-flow or equivalent engineering study when the lightweight design has long flow lengths, thin sections, multiple gates, filled resin, tight flatness, sealing interfaces or a large visible face. At minimum, the review should state the CAD revision, exact material data source, gate and runner assumptions, fill and pack behavior, cooling assumptions, predicted shrinkage or deflection, and limitations. Simulation can compare options; it cannot replace a production-intent trial.
Tooling decisions should also consider volume and transfer. A low-volume prototype tool may answer geometry questions but not prove multi-cavity balance, long-run wear or the final machine window. For production, agree cavity identification, process records, spare or repair strategy, inspection access and change-control triggers. A change in resin grade, fiber loading, colorant, tool insert, gate, cooling circuit, machine location or inspection method should trigger a documented review and, where risk warrants, renewed samples.
04
How should lightweight parts be validated before approval?
Set approval gates around the product risk, not around a supplier’s sample label. Gate 1 is concept feasibility: confirm the released requirements, baseline mass, proposed mass, material direction, load cases, environment, cosmetic zones and open design questions. Gate 2 is tool and process readiness: approve the DFM response, analysis assumptions, measurement plan, resin condition, mold concept and trial protocol. Gate 3 is production-intent evidence: inspect parts from relevant cavities and a stabilized condition, then compare mass, CTQs, flatness, fit, appearance and function against the agreed acceptance rules.
Dimensional results should state datums, part temperature, conditioning time, fixture or support method, instrument and sample basis. Flexible lightweight parts can read differently when clamped, probed or measured immediately after ejection. ISO 20457 provides a framework for plastics moulded-part tolerances and acceptance conditions, but the drawing, product standard and customer-specific requirements remain controlling [3]. Use a measurement-system review when a near-limit result could change the release decision.
Validation should include the use environment that matters to the application. Depending on the product, this may include temperature cycling, humidity conditioning, chemical exposure, assembly load, impact, fatigue, vibration, leak or retention testing. The exact test plan belongs to the product owner and applicable customer or regulatory requirements. Do not infer compliance from a resin datasheet, a simulation plot or a visually acceptable sample. Record deviations, containment, corrective action and the approver for each gate.
05
How can procurement compare supplier proposals fairly?
Normalize proposals against one controlled baseline. Ask each supplier to quote the same part revision, annual and peak volume, cavity assumption, exact material direction, color, packaging, inspection scope, sample quantity, tooling ownership and delivery boundary. Require a separate list of exclusions and assumptions. A lower tool or piece price may reflect a different gate, material, cavity count, inspection method or validation depth rather than a genuinely better lightweighting solution.
Request supplier evidence before award: a marked DFM response, material data and proposed alternative grades, shrinkage or warpage study, tooling concept, trial plan, dimensional report format, capability or repeatability evidence where relevant, and a change-control proposal. Evidence should be representative of the actual geometry and process. Generic machine lists, unrelated case studies or an unqualified percentage weight-saving claim do not establish fit.
Make approval conditional on closing the risk register. Procurement can compare total scope and commercial exposure; engineering can approve the structural and mold concept; quality can approve measurement and release evidence; the product owner can accept any stiffness, impact, appearance or service trade-off. If the lightweight concept cannot satisfy the requirement without an unresolved assumption, retain the baseline or redesign rather than treating the supplier’s recommendation as an automatic approval.

Practical takeaway
Before you move
to the next review.
- Define baseline and target mass together with stiffness, impact, fatigue, dimensional, assembly, appearance and environmental requirements; identify which are mandatory requirements and which are engineering recommendations.
- Name the exact resin grade, supplier, colorant, filler or recycled-content condition, moisture state and approved alternatives before comparing shrinkage or warpage predictions.
- Request a revision-controlled DFM and flow/pack/cooling review covering wall transitions, ribs, gates, vents, fiber orientation, ejection, cooling balance and measurement datums.
- Set approval gates for concept, tool/process readiness and production-intent samples, with defined stabilization, conditioning, inspection method, sample basis and deviation ownership.
- Obtain supplier evidence for mass, CTQs, stiffness, impact and relevant environmental or functional tests, and document change triggers for resin, tool, process, site or inspection changes.
FAQ
Common questions
Does reducing wall thickness always reduce injection molded part cost and cycle time?
No. Less material may reduce shot mass, but a thinner section can require higher filling pressure, a different gate, more stringent process control, slower filling or additional validation. Cooling, ejection, handling and inspection may remain the limiting steps. Confirm the result with the specified resin, geometry, volume and machine rather than assuming universal savings.
Are glass-filled plastics a reliable way to prevent warpage in lightweight parts?
Not universally. Glass fibers can increase modulus, but their orientation can make shrinkage directional and can increase warpage around gates, weld lines and flow turns. Tool wear, impact behavior, surface appearance and customer requirements also change. Approve a specific grade only after representative orientation, dimensional and functional evidence.
Can mold-flow software prove that a lightweight design will meet its drawing tolerances?
No. Simulation can compare filling, packing, cooling, orientation and predicted deflection using stated assumptions. It does not replace molded samples, calibrated inspection, conditioning, functional testing or production-process evidence. Ask the supplier to show inputs, limitations and how the prediction will be checked at trial.
What should an OEM do if the first lightweight samples warp?
Contain the affected samples and preserve the tool, resin and process records. Compare the distortion by cavity, orientation, wall region, gate and cooling condition, then review material moisture, packing, cooling, ejection and measurement setup. Possible actions include geometry, gate, cooling, process or material changes, but each can create new trade-offs and should pass the agreed engineering approval gate before release.
References
Source material
- [1] Autodesk Moldflow Advisor: Warpage problems
- [2] BASF: Injection-Molding Problems in Engineering Thermoplastics—Causes and Solutions
- [3] ISO 20457:2018, Plastics moulded parts—Tolerances and acceptance conditions
- [4] Autodesk University: Optimize Plastic Part Designs—Injection Molding Simulation in Autodesk Fusion 360
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.