
Thin-wall medical injection molding makes sense when a thin section is required by the part’s function, package, fluid path, ergonomics or material efficiency, and the team can show that the chosen geometry, resin, feed system, cooling approach and inspection plan are controllable. It is not justified merely because a smaller wall appears cheaper or because a generic minimum thickness has been met. Thin walls can make flow, cooling, weld-line, ejection and dimensional risks more sensitive, so the decision should be made against the finished part’s requirements and evidence plan.[1]
For a medical component, treat thin-wall molding as a controlled trade-off: preserve the required function and envelope, but do not trade away fill evidence, material identity, tool maintainability or inspection capability. Visuals in this guide are illustrative engineering images only; they do not depict an InjeForm customer part, validated process or production result.
01
Start with the reason the wall must be thin
First identify the constraint that makes a thin wall valuable. It may reduce the envelope of a handheld diagnostic component, preserve a fluid-path opening, support a disposable format, allow a membrane or flex feature, or meet an assembly clearance. If the only reason is an assumed unit-cost saving, compare a slightly thicker and easier-to-fill design before committing to the higher process sensitivity. A wall that is thin in one resin and flow length may be ordinary in another, so avoid a universal threshold as a release rule.[1]
Map the wall together with ribs, bosses, corners, ports, windows, seals and mating faces. A local transition can be more important than the nominal wall. Mark patient-, sample- or reagent-contacting surfaces, loaded areas, cosmetic zones and dimensions that affect assembly. FDA’s ISO 10993-1 guidance frames biological evaluation around the device, its materials and the nature of body contact; a molding review therefore cannot decide biological suitability from thickness alone.[5]
02
Test filling and cooling as one geometry decision
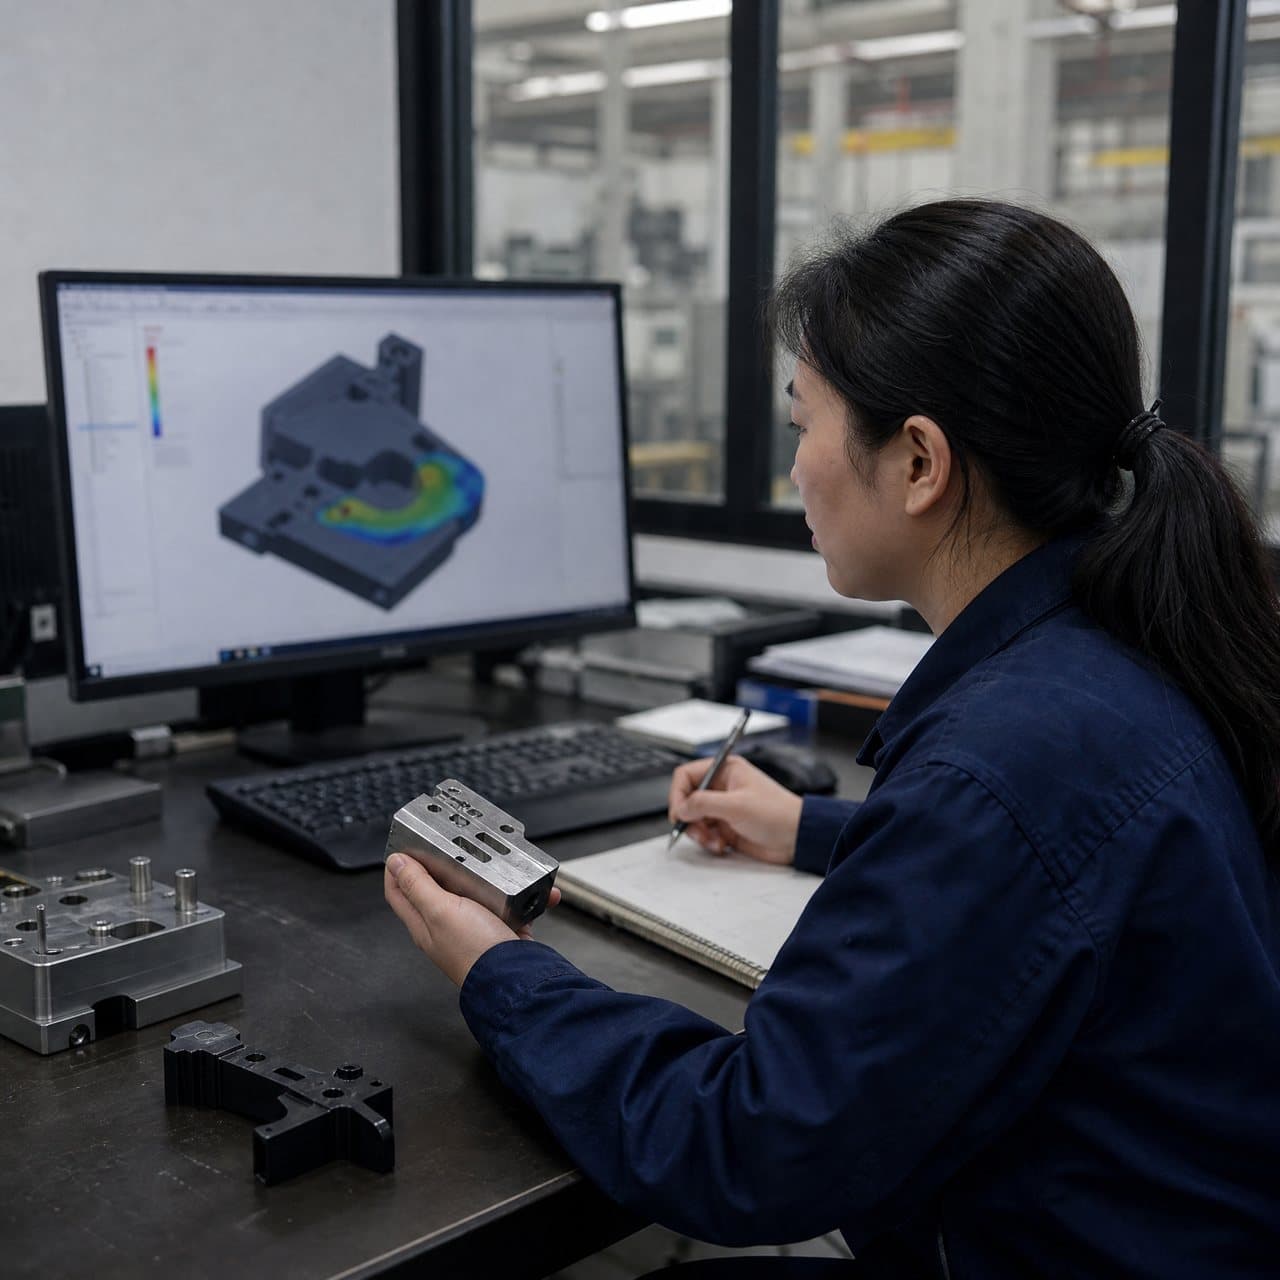
Thin sections lose heat quickly as the melt advances, while long flow paths, restrictive gates, sharp transitions and trapped air can make filling less forgiving. A complete-fill simulation is not a finished-part approval. Ask which CAD revision, resin data, gate, runner, mold-temperature assumptions and process window were represented. Review fill progression, pressure demand, flow-front temperature, air traps and predicted weld or meld lines. Autodesk notes that flow fronts which cool before meeting may not interfuse well, creating a weakness or visible line.[2]
| Decision question | Evidence to request | Buyer response |
|---|---|---|
| Can the thinnest region fill consistently? | Part-specific fill study, last-to-fill location, pressure and flow-front-temperature assumptions, plus trial checks. | Retain the design, revise the feed path or revise the wall and record the remaining uncertainty. |
| Will cooling create distortion or unstable dimensions? | Wall-transition map, cooling concept, expected cycle sensitivities and dimensional checks after agreed conditioning. | Core out mass, smooth the transition, improve cooling access or define a controlled process study. |
| Where will air, weld lines or gate evidence appear? | Predicted convergence and air-trap areas, venting proposal, gate location and allowed witness zones. | Move the feature or gate, add the appropriate tool detail or accept it only with a product-specific criterion. |
| Can the thin part be ejected without damage? | Draft direction, ejection layout, release force assumptions and inspection of fragile edges or ports. | Add draft or radii, change ejection support, or reconsider the geometry before steel release. |
03
Choose material for the part, not for the label
Material selection should balance flow, stiffness, toughness, chemical exposure, temperature, sterilisation or cleaning conditions, surface requirements and the product owner’s qualification route. Some resins can fill thin geometry more readily than others, but easier flow does not automatically mean better dimensional stability, weld-line performance or compatibility with the intended use. Protolabs identifies thin-wall risks including incomplete formation, uneven cooling, warp, weak knit lines and cosmetic inconsistency, and also cautions that material choice depends on geometry and application.[1]
For medical work, record the exact manufacturer and grade direction, colorants or additives, lot or batch controls where required, drying or conditioning assumptions, and the response to a material change. “Medical grade” is not a complete approval decision. ISO 13485 is a quality-management standard for organisations involved in medical devices and related services, while the U.S. QMSR applies to finished-device manufacturers within its scope; neither statement by itself proves that a thin molded component is suitable for a particular device or market.[3] [4]
04
Make tooling choices that preserve process and inspection options
Tooling should be reviewed around the thin section’s feed and release needs. Gate type and location affect flow direction, packing access, vestige and weld-line position. Runner balance matters in multi-cavity tools, while cooling-channel access, venting, steel support and shutoff durability affect repeatability and maintenance. Protolabs describes gates, runners, cooling channels and ejectors as integral mold features, and links wall consistency with cooling and warpage risk.[1] Avoid choosing a cavity count or hot-runner concept on piece price alone if it removes practical access to the critical wall or makes cavity-to-cavity comparison harder.
Before tool release, identify replaceable inserts, vent-cleaning access, gate maintenance, ejection support and any geometry likely to wear or flash. Then connect those choices to the inspection plan. A thin edge, port, seal land or snap may need a fixture, optical method, CMM setup or functional check that is not obvious from a general dimensional report. Quote-oriented CTA model: send the controlled CAD and drawing revision, wall map, resin direction, annual and launch volumes, critical interfaces, allowed gate zones and requested sample evidence, then ask the supplier to return assumptions, tooling options, inspection scope and open risks in the quotation.
05
Define inspection evidence before deciding that it makes sense
The right question is not whether a thin part can be measured once. It is whether the agreed method can distinguish acceptable variation from a failure of fit, flow, sealing, appearance or function. Define critical-to-quality characteristics, datum setup, part conditioning, sample or lot basis, instrument or fixture, visual standard and reaction plan. Inspect the thin wall where it drives the product decision, but also inspect the neighboring features that can move when cooling or packing changes.
Separate engineering feasibility from design transfer, validation and routine release. A first sample may support a geometry decision while leaving process capability, sterilisation exposure, biocompatibility, packaging and market-specific obligations open. FDA states that QMSR applies to finished device manufacturers that intend commercial distribution and incorporates ISO 13485:2016 by reference; a component supplier should therefore document its agreed contribution rather than imply finished-device compliance.[3] If the evidence cannot support the next decision, the thin-wall route is not ready even when the samples look acceptable.

Practical takeaway
Before you move
to the next review.
- State the functional, packaging, fluid-path or assembly reason the wall must be thin, and compare an easier-to-fill alternative.
- Provide a controlled wall map with gates, flow length, transitions, ribs, ports, seals, cosmetic areas and critical interfaces identified.
- Request a part-specific review of filling, flow-front temperature, air traps, weld lines, cooling, ejection and tooling maintenance access.
- Name the exact material route, exposure assumptions, additives or colorants, change boundaries and the owner of medical or regulatory decisions.
- Agree inspection methods, conditioning, sample or lot basis, acceptance criteria and reaction plans before treating a sample as evidence.
FAQ
Common questions
Is there a universal minimum wall thickness for medical injection molding?
No. A useful decision depends on the resin and grade, flow length, gate and runner concept, mold temperature, geometry, required function, surface expectations and inspection method. Use any published guideline as an early design prompt, not as a universal approval value.[1]
Does a medical-grade resin make a thin molded part suitable for a medical device?
No. The product owner must assess intended use, contact and exposure, formulation and processing route, finished configuration, validation and applicable market requirements. A resin description or supplier document can support the material route but does not establish finished-device suitability.[5]
Can higher injection speed solve a thin-wall short shot?
Not reliably. Speed, melt and mold temperature, gate restriction, venting, material condition, flow length and geometry can interact. Increasing speed can introduce other risks, so compare the suspected mechanism with simulation, tooling review and controlled trial evidence rather than applying a blanket setting change.[2]
Should thin-wall medical parts always use a hot runner or multi-cavity tool?
No. The appropriate feed and cavity strategy depends on volume, material, gate evidence, balance, maintenance, validation scope and inspection capability. A more complex tool can improve one objective while making another harder to control.
What should procurement ask for in a thin-wall molding quotation?
Ask the supplier to state the assumed CAD revision, resin and grade, wall-risk areas, gate and runner concept, cavity count, cooling and venting approach, expected trial evidence, inspection method, exclusions, change boundaries and the decisions the quote does not support. This makes unlike technical scopes easier to compare.
References
Source material
- [1] Protolabs, “Thin Wall Injection Molding Tips and Considerations.”
- [2] Autodesk, “Troubleshooting weld lines and meld lines.”
- [3] U.S. Food and Drug Administration, “Quality Management System Regulation (QMSR).”
- [4] International Organization for Standardization, “ISO 13485 — Medical devices.”
- [5] U.S. Food and Drug Administration, “Use of International Standard ISO 10993-1.”
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.