
Snap hooks, clips and retainers are small molded features with outsized influence on assembly time, rattle, serviceability and field failure risk. A hook may capture a cable, panel, tube or cover; a clip may provide a push-in or slide-in attachment; a retainer may locate a mating part while resisting vibration or handling loads. For an overseas OEM, the sourcing question is not simply whether a supplier can mold the shape. It is whether the complete interface, resin, tool strategy, process window and approval evidence fit the released product requirement.
Start by separating requirements from recommendations. The product team should define the mating-part range, engagement direction, retention objective, installation and removal intent, environment, critical datums and acceptance method. The molder may recommend a resin grade, arm geometry, draft, gate, parting line, side action, cavity count or inspection plan. Those recommendations depend on the selected grade and colour, geometry, tooling, machine, environment, volume and customer specification. A data sheet, CAD review or first-off sample alone does not approve a finished snap feature.
Treat every snap feature as a controlled interface. The required retention, assembly force, deflection, service cycles and environment belong in the product specification; the supplier's geometry and tooling proposals must be reviewed against those requirements before tool release.
01
1. What should buyers define before requesting a quotation?
Provide the controlled CAD and drawing revision together with the actual mating part or an agreed interface model. Mark the capture surface, lead-in, return face, relief window, root transition, seating surface, release access, assembly direction, removal direction and no-go zones for gates, ejectors or parting lines. A nominal panel thickness or diameter is not enough; include its tolerance, coating, burr condition, hardness or compliance where those affect fit.
State the function in measurable terms. The requirement may be a minimum retention force in a named direction, a maximum insertion force, a permitted deflection, a defined number of assembly or service cycles, a no-rattle condition, a pull-out load, or dimensional fit at temperature and humidity. If the product is intended to be permanent, do not quietly use a reusable-clip assumption. If service removal is required, identify tool access and the acceptable release method.
Give the supplier the use environment and risk context: temperature range, humidity, fluids, UV, vibration, impact, cleaning chemicals, sustained load, mating frequency, packaging and installation handling. Ask for an assumptions log that identifies missing mating data, proposed resin and colourant, flow direction, tool pull direction, undercuts, side actions, measurement condition and any exclusions from the quotation. Requirements are controlled inputs; supplier suggestions remain recommendations until approved.

02
2. How do snap hooks, clips and retainers compare?
A snap hook usually uses a flexible arm and a return face to capture a feature. A clip may be a cantilever, U-shaped, torsion or annular arrangement, or a molded feature combined with a metal stud or panel. A retainer is a broader functional term for a part that locates or holds another component and may use one or more hooks, ribs, windows, tangs or secondary locks. Select by load path and assembly sequence, not by catalogue name.
The comparison below is a screening framework. It does not establish universal force, life, tolerance or resin limits. The same feature can behave differently when its arm length, root radius, wall transition, fiber orientation, mating material, friction, conditioning and temperature change.
| Feature type | Useful when | Typical trade-off to review | Buyer evidence before approval |
|---|---|---|---|
| Cantilever snap hook | A one-direction flexing arm can engage a slot, bead or panel edge | Root strain, creep, fatigue, insertion force and release access | Strain or deflection review, molded-part fit check and functional force test |
| U-shaped or wraparound clip | The design needs longer effective flexibility or capture around an edge | Tool access, local wall thickness, deformation during assembly and trapped geometry | Sectioned DFM review, tool concept, assembly trial and retention test |
| Torsion or annular feature | The load can be carried through rotation or circumferential flexure | Stress distribution, friction, ovality, mating-part variation and release force | Dimensional study, rotational or insertion test and environmental check |
| Retainer with secondary lock | Primary capture must be backed up against vibration, impact or service handling | Extra assembly step, tolerance stack, lock visibility and incorrect engagement | Error-proofing review, end-of-line check and assembled-system validation |
03
3. How should resin and geometry be selected?
Choose a candidate grade from the duty, not from the feature name. A flexible unfilled thermoplastic may suit a short-term, low-load clip, while an engineering grade may be considered where stiffness, heat or dimensional stability controls the design. Filled materials can change stiffness and shrinkage direction, but they may also reduce allowable flexure, alter weld-line behavior and make the feature more sensitive to flow orientation. Moisture conditioning, colourants, recycled content, additives and grade substitutions can also change performance.
The snap arm should be reviewed as a molded beam or compliant mechanism, with the highest strain normally near the root. Covestro's snap-fit guide describes cantilever, U-shaped, torsion and annular joints and emphasizes that permissible undercut depends on material and geometry [1]. Use calculations or simulation to screen the concept, then test the production-intent molded feature. Do not copy a generic strain percentage, fillet ratio, gap or tolerance into the drawing without checking the exact resin, geometry and condition.
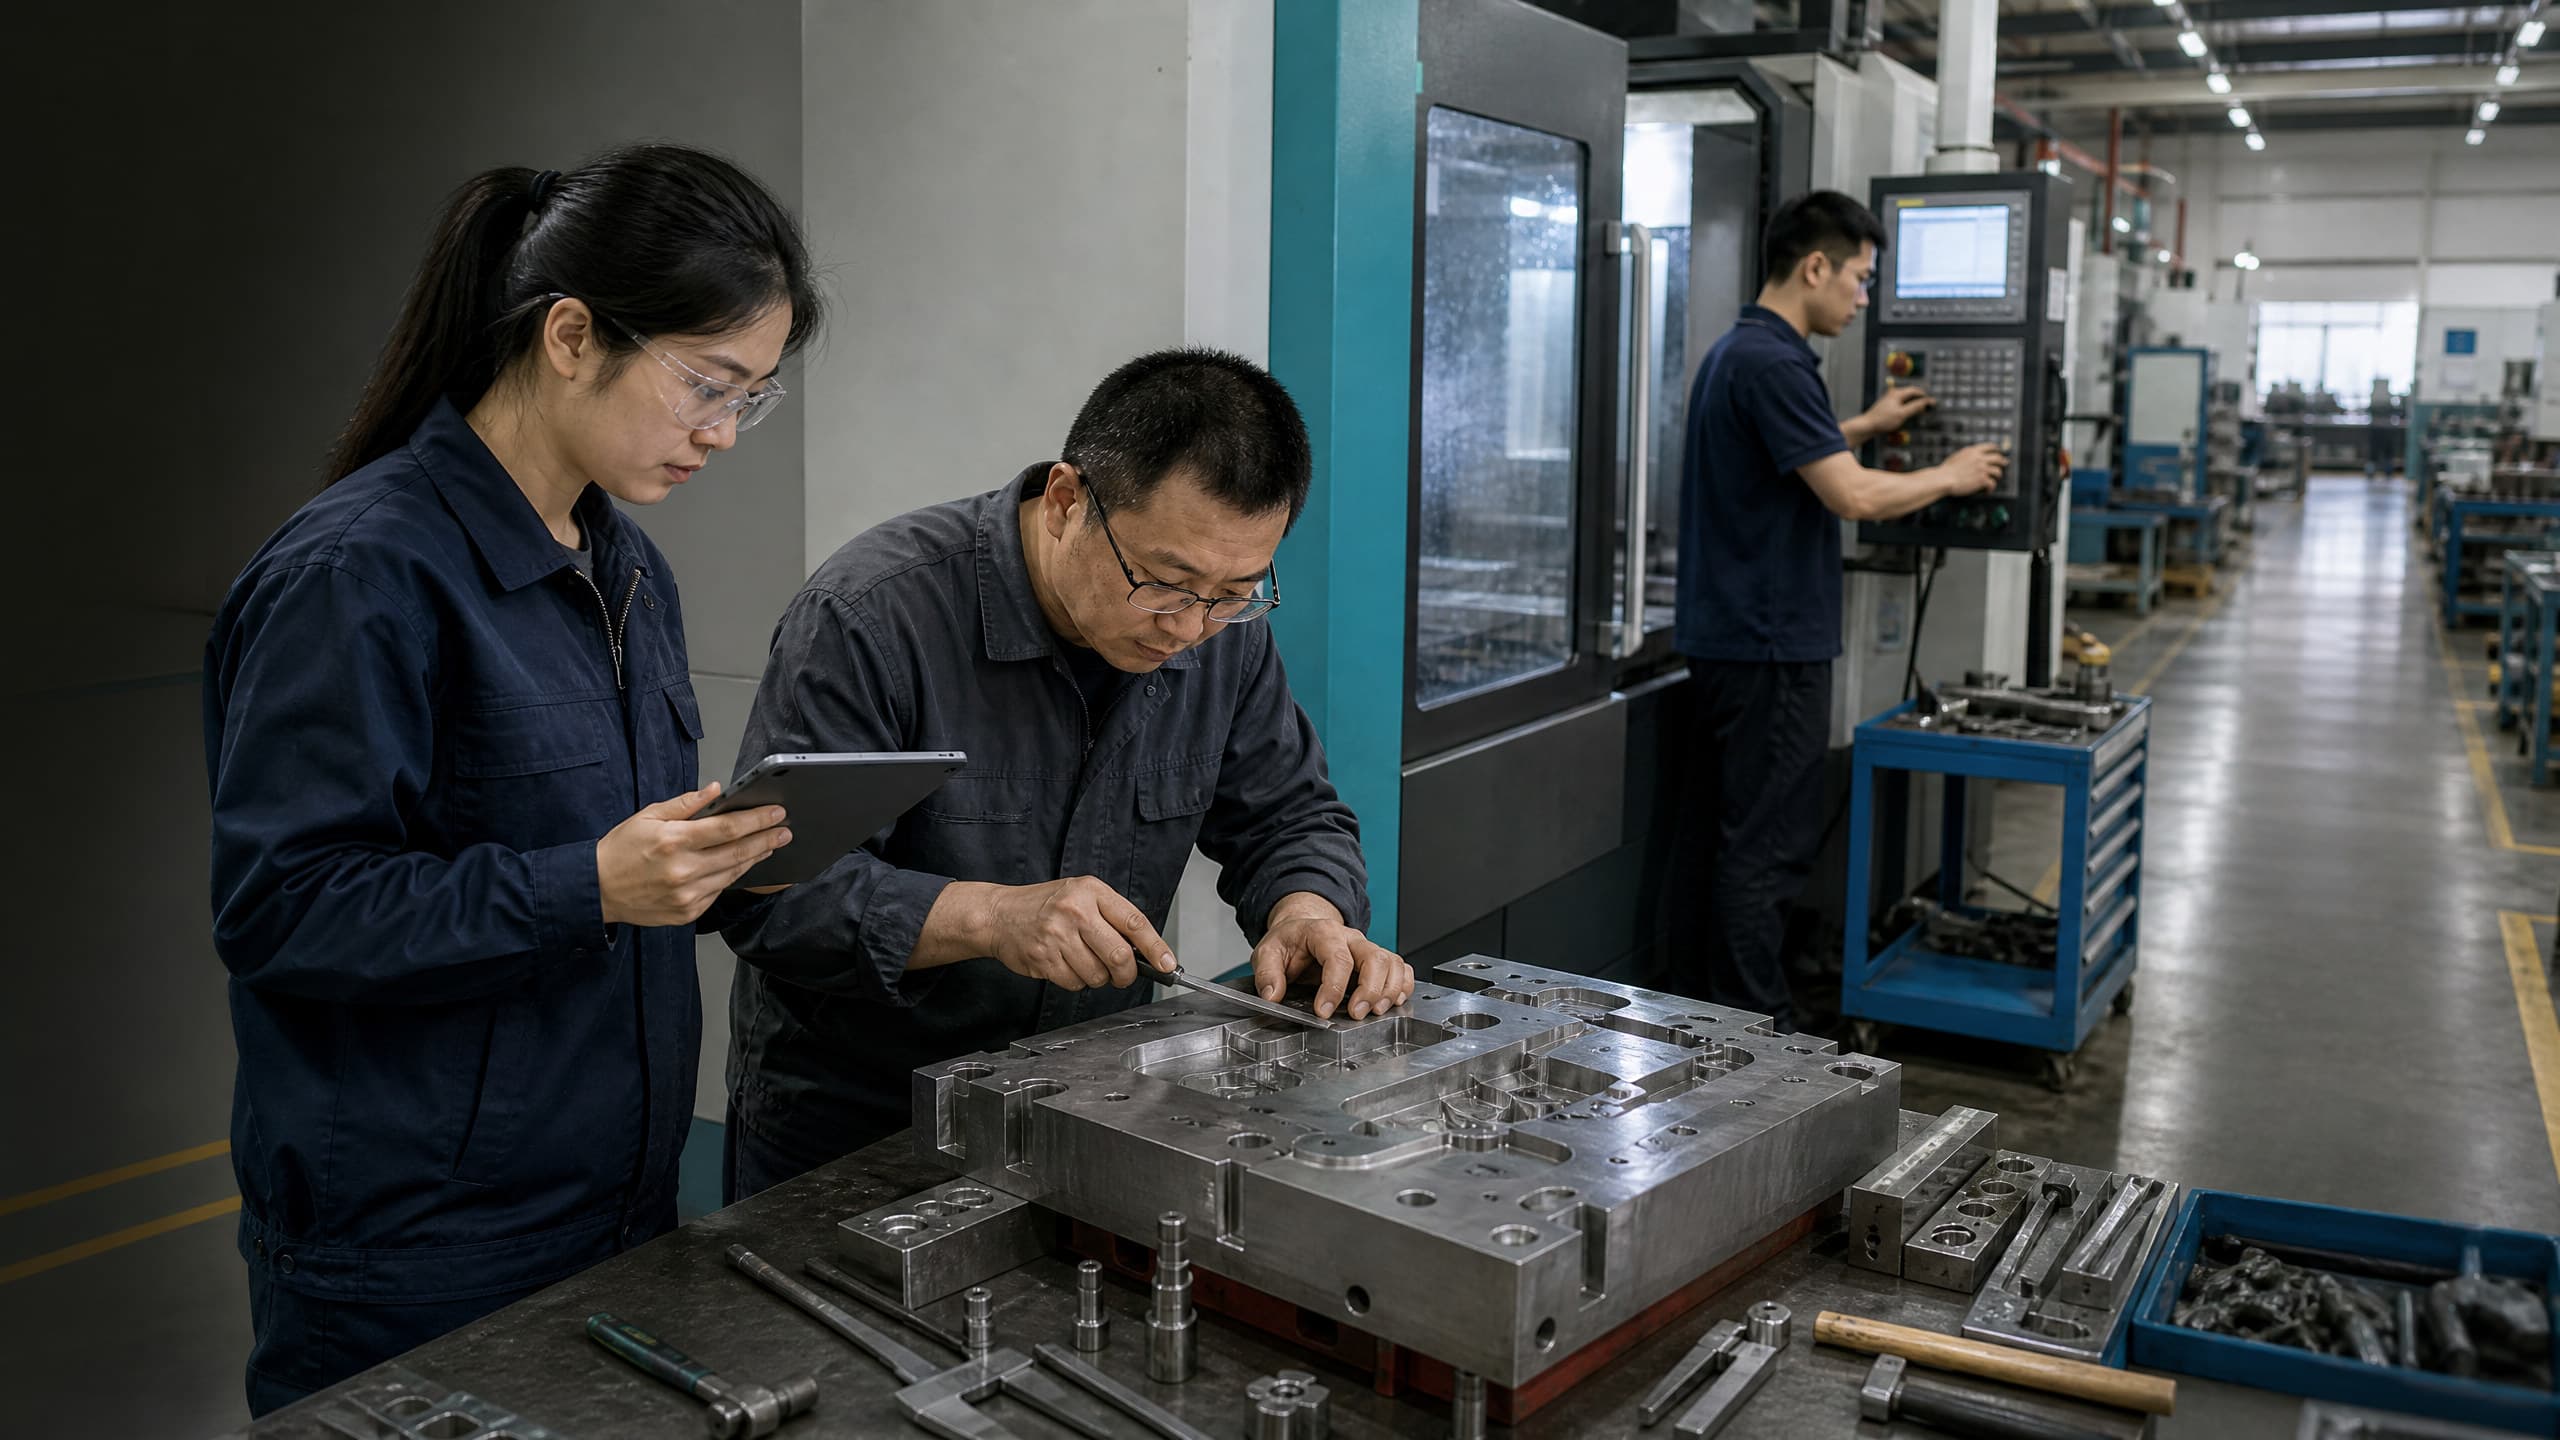
Geometry and molding are linked. Smooth root transitions, controlled wall changes, adequate draft and a clear ejection route are recommendations to review, not universal guarantees. Gate location and flow direction can affect weld lines, orientation and warpage. A relief opening may make a clip moldable with a sliding shutoff; another undercut may require a side action, hand-loaded insert or a redesign. These choices can change tool complexity, maintenance, cycle behavior and piece cost, so ask for a marked DFM and mold-concept review before tooling approval.
04
4. What tooling and process questions affect supply risk?
Ask the supplier to show the mold opening direction, parting line, shutoffs, slides or lifters, inserts, vents, gates, ejectors and any hand-loaded elements. Protolabs notes that snap features often need a sliding shutoff aligned with mold opening, while other undercuts may call for a side action or insert [2]. The correct solution depends on the released geometry and tool design; a quotation that says 'standard mold' without an undercut plan is incomplete.
Review whether the chosen tool concept protects the functional interface. A parting line across a latch face, an ejector witness on a seating surface, a weld line at a flexing root or a gate vestige in a hand-contact area may be unacceptable even if the part is dimensionally close. Define cosmetic and functional witness limits by zone, and identify which features require datum-based inspection.
Do not accept universal promises on tolerance, cycle time, price or tool life. Molding results depend on resin rheology, moisture, cavity balance, machine capability, cooling and venting, mold steel, maintenance, volume and process control. Request the proposed material traceability route, process-control plan, cavity identification, measurement method, sampling plan and change-notification rules. For multi-cavity tools, require evidence that cavity-to-cavity variation is included in the approval plan.
05
5. Which supplier evidence and approval gates are practical?
Use staged approval rather than treating a prototype as production approval. At the design gate, review the controlled interface, load cases, resin shortlist, tolerance stack, assembly sequence, DFM findings and risk register. At the tool-release gate, approve the mold concept, parting line, undercut solution, gate and ejector locations, steel and maintenance assumptions, and any drawing changes. Record deviations as explicit dispositions.
At first trials, request parts from the intended resin grade, colour and process route, with cavity identification and processing records. Check fit to the real mating parts, insertion and release force, retention in the specified direction, visible damage, root marks, flash, short shots, warpage, critical dimensions and assembly error modes. ASTM D638 explains that tensile data vary with specimen preparation, speed and environment and cannot by themselves predict applications with different load-time scales or environments [3]. Use material data and coupon tests as inputs, not as substitutes for part-level evidence.
Before production release, define the acceptance report and open-item closure. Depending on risk, this may include dimensional capability, assembled retention, repeated-cycle testing, vibration or impact, temperature and humidity conditioning, chemical exposure, packaging simulation and an agreed visual standard. ISO 20457 provides a framework for tolerances and acceptance conditions for plastic molded parts, but the buyer still needs product-specific critical dimensions, datums, measurement conditions and functional limits [4]. Release only when the evidence matches the approved configuration and customer specification.

Practical takeaway
Before you move
to the next review.
- Provide revision-controlled CAD, drawings, mating-part data, datums, capture dimensions and the intended assembly and service directions.
- Define measurable retention, insertion, release, deflection, cycle, environmental and cosmetic requirements; do not substitute a generic clip label.
- Request a named resin grade and colour route with data sheet, conditioning assumptions, traceability, substitution rules and part-specific risk review.
- Require a marked DFM and mold concept showing parting line, shutoffs, side actions, inserts, gates, vents, ejectors and maintenance assumptions.
- Set approval gates for design, tool release, first trial and production intent, with functional tests on the molded part and actual mating components.
FAQ
Common questions
What is the best plastic for injection molded snap hooks and clips?
There is no universal best plastic. The candidate grade depends on required flexure, sustained load, temperature, chemicals, humidity, impact, mating materials, assembly cycles, dimensional stability and customer restrictions. Compare named grades using application-relevant evidence, then validate the production-intent molded feature. A resin family name or data sheet alone does not approve a snap hook.
Do snap hooks always require slides or side actions in the mold?
No. Some hooks can be formed with a relief opening, shutoff or pull direction that allows the mold to open cleanly. Other undercuts require a side action, lifter, insert or a geometry change. The answer depends on the feature orientation, parting line, draft, ejection and tool concept. Ask for a marked mold review rather than assuming a standard tool or a universal tooling surcharge.
How can a buyer verify that a molded retainer will not lose its grip?
Define the mating-part range, load direction, installation condition, service cycles and environment first. Then require a part-level test using production-intent material, geometry and mating components, with agreed fixtures, conditioning, force measurement and pass/fail limits. Screening calculations and material data can identify risk, but they do not establish retention life under every temperature, chemical or vibration condition.
Should snap hooks be dimensioned with a generic plastic tolerance?
Avoid a blanket tolerance when a feature controls assembly or retention. Mark functional dimensions and datums, define the measurement condition and analyze the mating stack. ISO 20457 can support the discussion of molded-part tolerances and acceptance conditions, but the correct limit remains specific to the resin, geometry, tool, process, measurement method and customer requirement.
References
Source material
- [1] Covestro, Snap-Fit Joints for Plastics: A Design Guide
- [2] Protolabs, 5 Ways to Master Complex Features in Injection-Molded Parts
- [3] ASTM D638-22, Standard Test Method for Tensile Properties of Plastics
- [4] ISO 20457:2018, Plastics Moulded Parts — Tolerances and Acceptance Conditions
This guide is general information for early procurement and engineering discussion. It does not replace product-specific DFM, qualification, validation, regulatory assessment or legal advice.